Более 24 лет опыта и знания международных стандартов, Технологические изменения и промышленные системы, мы стремимся Компания Seds предоставляет лучшие и экономичные решения для своих клиентов.
Metal Coil Slitting Line: A Complete Buyer’s Guide for Roll Forming Factories
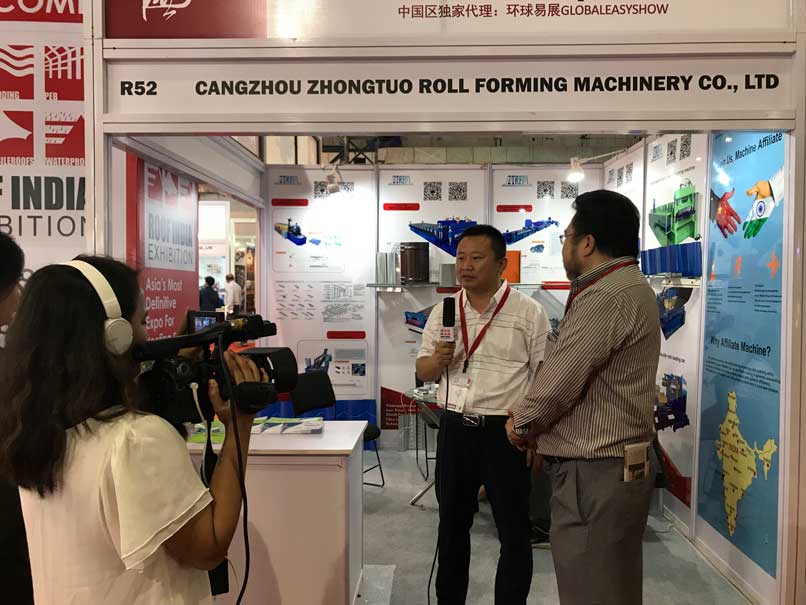
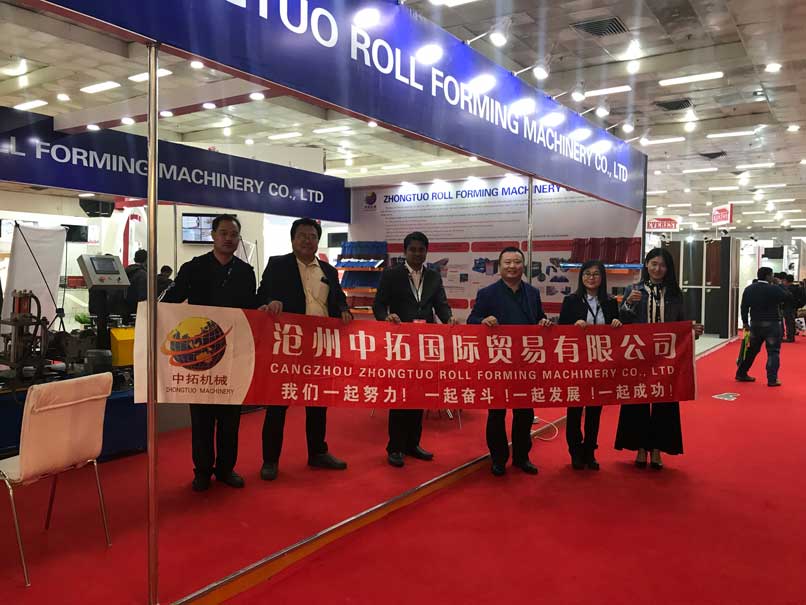
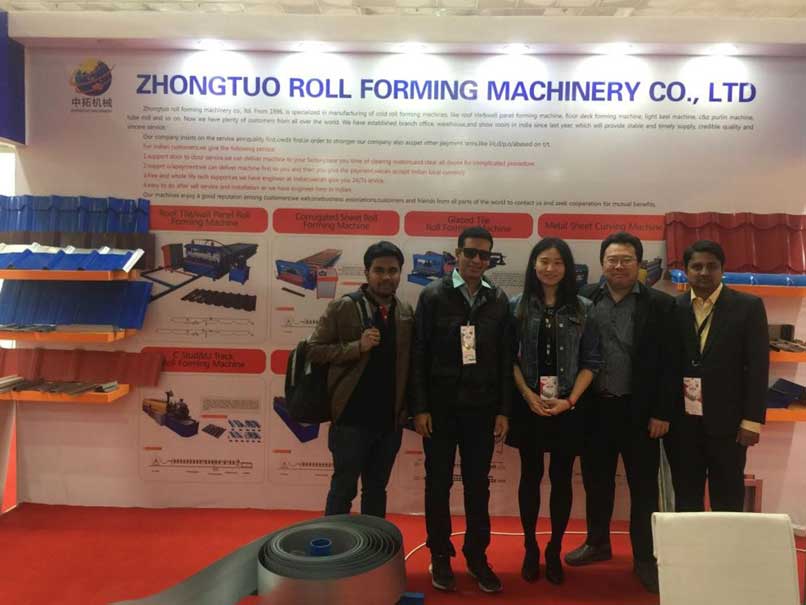
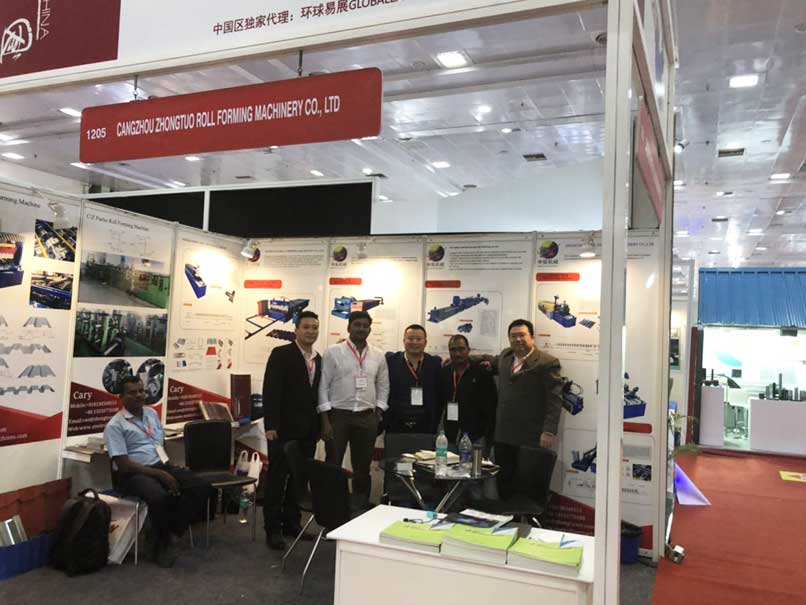
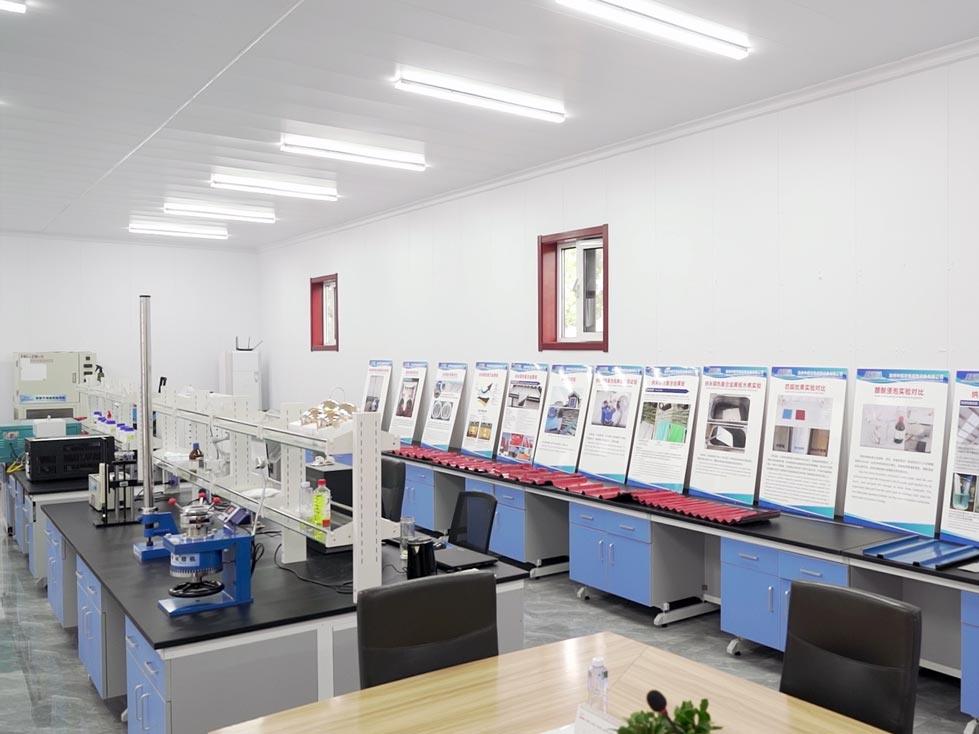
Компания Cangzhou Zhongtuo Roll Forming Machinery Co. Ltd родом из Хэбэй-Китай. Это производитель, занимающийся разработкой и производством. различные типы машин для холодной прокатки. Мы являемся заводом с многолетней историей, занимающимся разработкой и производством валковых формовочных машин с 2006 года. Мы можем производить следующие машины: машина для производства черепицы, машина для производства обрешетки, машина для производства киля из легкой стали, машина для тиснения металла, машина для формирования дверных систем, машина для формирования потолочных систем, высокочастотная машина для сварки труб, линия продольной резки, линия для резки по длине, машина для формирования полочных систем, машина для формирования настила пола, линия для производства цветной каменной плитки, машина для горячей ламинации и т.д.
Metal Coil Slitting Line: A Complete Buyer’s Guide for Roll Forming Factories
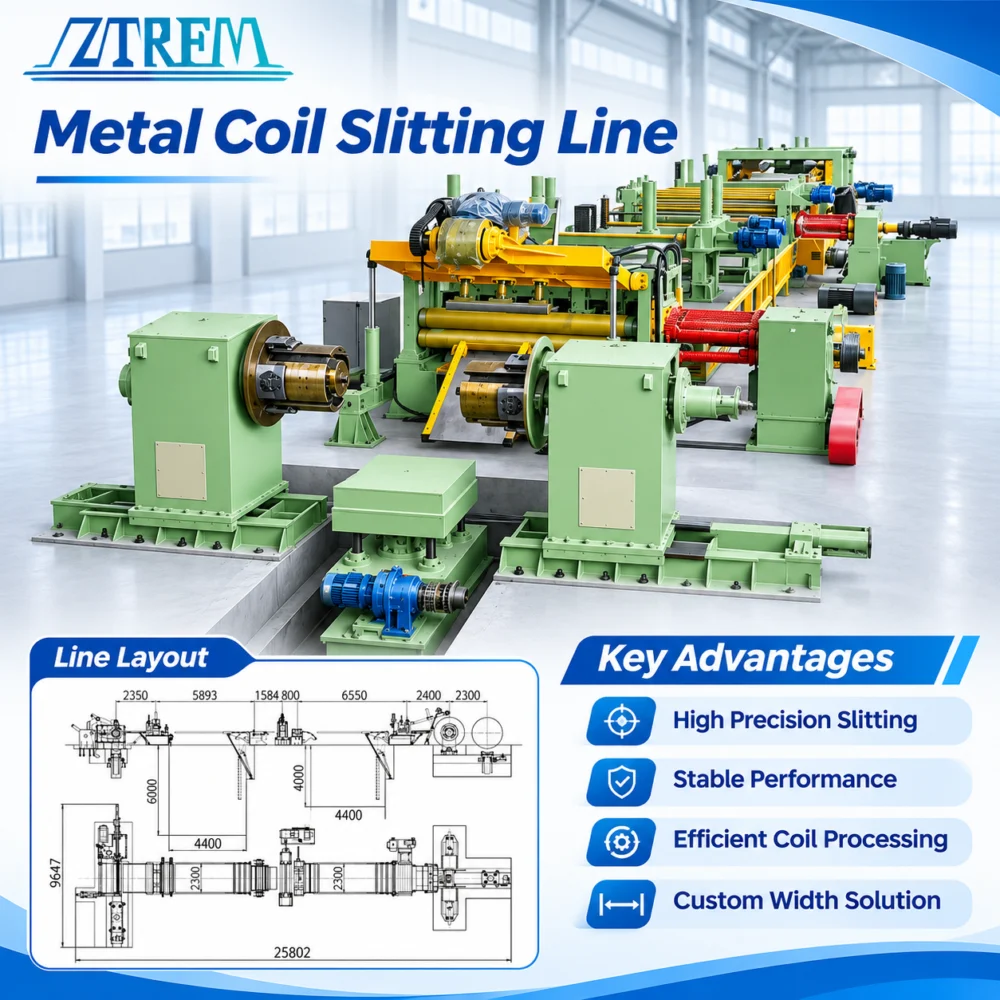
A slitting line (also called longitudinal slitter line) is the core upstream coil processing equipment for every metal roll forming workshop. It cuts wide master metal coils longitudinally into multiple narrow strips, then rewinds those strips into compact slit coils ready for your roof panel, ridge cap, purlin, guardrail and cable tray roll forming machines. If you run a roll forming business, matching your raw coil width to your forming profile is the first step to stable output, low waste and consistent finished quality.
Many roll forming operators buy pre-slit strips from service centers. While this saves upfront investment, it locks you into fixed widths, longer lead times, extra freight cost and risk of surface scratches during transit. Adding your own slitting line lets you adjust strip widths on demand, match coil color and thickness perfectly, and cut waste rates down significantly. This guide covers working principle, main line sections, critical specs, material options, common pitfalls and what to check before requesting your quotation.
Metal Coil Slitting Line: A Complete Buyer’s Guide for Roll Forming Factories
How a Metal Slitting Line Works
The whole slitting process runs continuously in one flow:
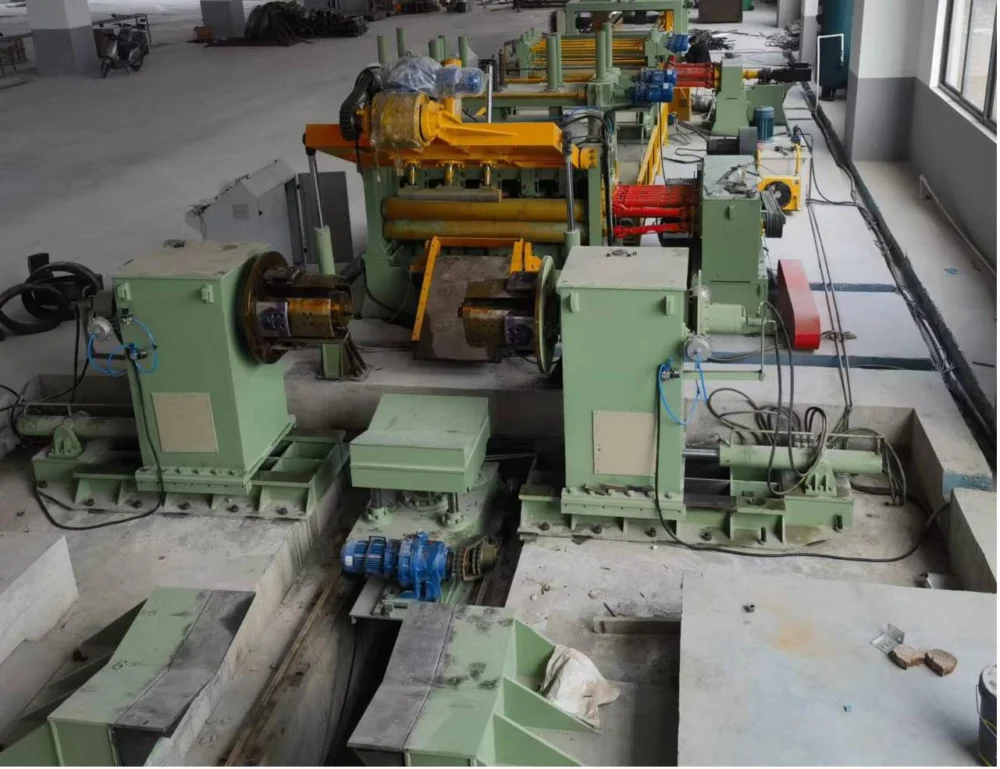
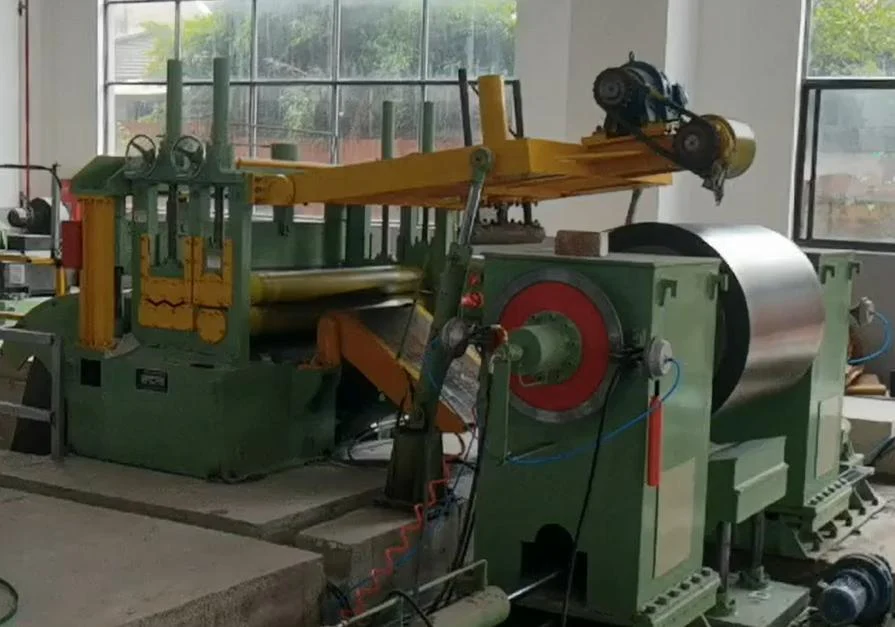
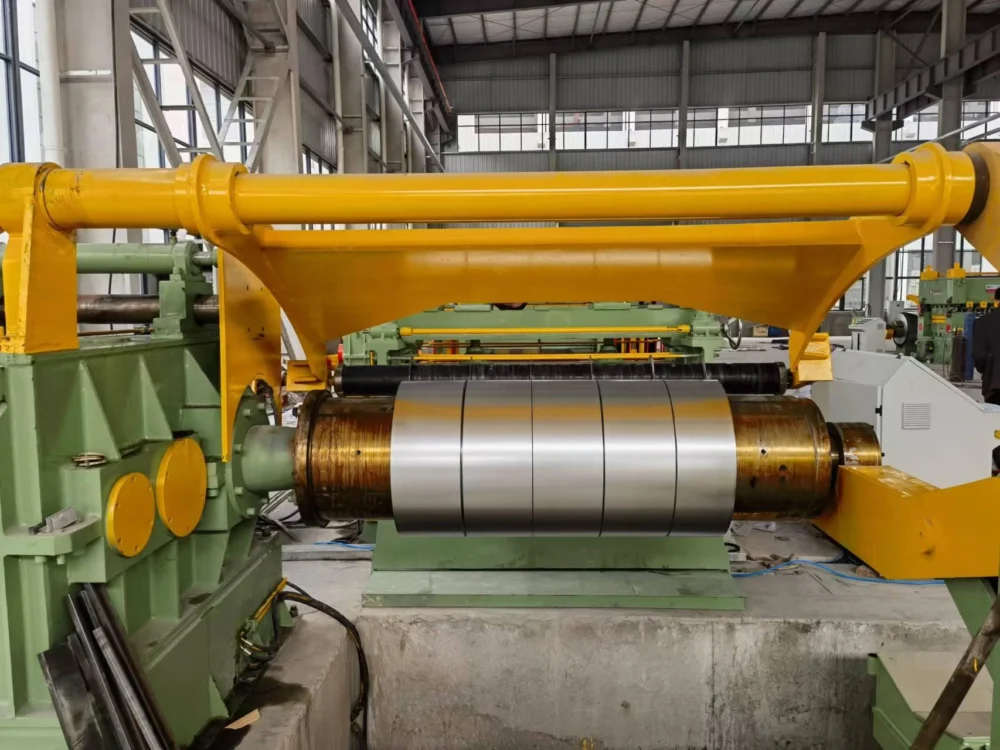
Decoiling: The heavy master coil is loaded onto the decoiler, unwound steadily with controlled tension to avoid snaking or scratching the coated surface. Hydraulic decoilers are standard for heavy coils above 3 tons; manual decoilers suit light-duty, small-batch production.
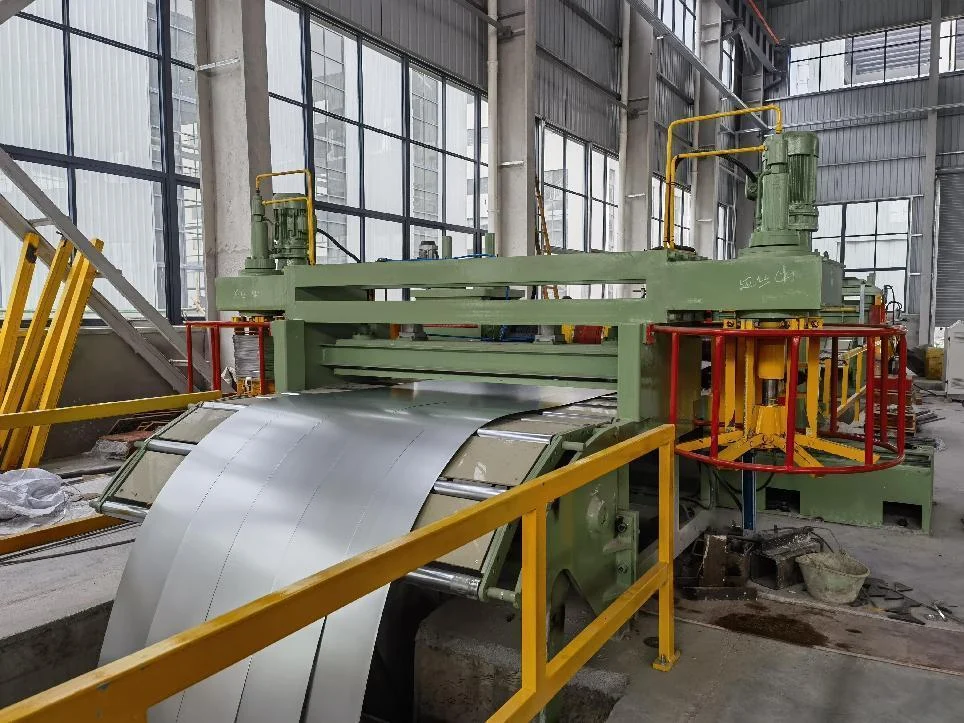
Leveling & Side Guiding: The strip passes through pinch rolls and leveler rollers to remove coil camber. Side guides and EPC edge correction keep the strip centered before entering the slitter head, which is critical for uniform width tolerance.
Rotary Slitting: A set of upper and lower circular knives shear the metal lengthwise. Knife spacing is adjusted to match your target strip widths. The edge trim scrap is separated and wound or chopped for recycling.
Tension Stand & Separator: This section creates stable strip tension to prevent loose winding, strip overlap and surface marks. Separators keep individual narrow strips apart before recoiling.
Recoiling: Finished narrow strips are rewound into tidy slit coils by the recoiler. Good tension control ensures tight, stable coils that feed smoothly into your roll forming machine without tower winding or collapse.
Main Components of a Full Slitting Line
The quality gap between cheap and heavy-duty slitting lines mostly lies in these assemblies:
Разматыватель: Hydraulic expansion type, coil car optional for fast coil loading. Rated coil weight and inner diameter must match your local master coil stock.
Leveler Unit: Multi-roller leveler for correcting camber and waves. Essential for PPGI, galvalume and thin coated steel to avoid burrs and uneven slitting.
Slitter Head: The heart of the line. Knife arbor diameter, knife material, spacing precision and bearing quality decide cutting edge quality and service life. D2 / Cr12MoV tool steel knives are widely used for long working life.
Scrap Winder / Scrap Chopper: Handles edge trim. Scrap choppers are popular for thin roofing coils; scrap winders work better for thicker carbon steel.
Tension Group & Separator Discs: Separators stop strips from rubbing each other, which is vital for prepainted coils to avoid paint scratching.
Recoiler: Hydraulic expansion, with friction or servo tension control. Larger recoiler capacity reduces coil change frequency.
PLC Control System: Touch screen to set strip width, speed, counter and EPC parameters. Multi-language interface and remote diagnostic support are helpful for overseas users.
Safety Guards & Emergency Stop: Full protective guards for rotating knives and moving parts, compliant with standard industrial safety requirements.
Metal Coil Slitting Line: A Complete Buyer’s Guide for Roll Forming Factories
Typical Applications for Roll Forming Manufacturers
This slitting line is built to pair with your roll forming production lines, widely used for:
Metal roof panel, ridge tile and gutter strip production
C purlin, Z purlin, solar bracket and cable tray raw strips
Highway guardrail, floor decking, fence and door frame profiles
Steel service centers, metal fabrication workshops and steel trading companies
It processes galvanized steel, galvalume (aluzinc), PPGI prepainted coil, cold rolled carbon steel, aluminum coil and thin stainless steel. For coated roofing coils, the line must run with low-mark rollers and gentle tension to protect the paint surface.
Key Specifications You Need to Confirm Before Quotation
Suppliers deliver very different machines under the same “slitting line” name. Prepare these data first so you can compare quotes fairly:
Material thickness range: Common roofing lines cover 0.25 mm – 1.2 mm; heavy-duty lines handle up to 3 mm or thicker carbon steel
Max master coil width: 1250 mm, 1300 mm, 1500 mm are the most popular options
Max coil weight: 3 ton, 5 ton, 8 ton or custom
Inner coil diameter: Usually 508 mm or 610 mm
Minimum slit width you require: This decides knife arbor layout and separator configuration
Required slitting tolerance: Standard ±0.3 mm, high precision ±0.15 mm
Line speed: 20–80 m/min for light roofing coil; heavy steel lines run slower for stable cutting
Power supply: Local voltage, phase and frequency
Floor space and container loading plan
A common mistake buyers make is overbuying speed. If your downstream roll forming machine only runs 12 m/min, a 60 m/min high-speed slitter will sit idle and add unnecessary cost. Match slitting speed to your forming line capacity instead.
Metal Coil Slitting Line: A Complete Buyer’s Guide for Roll Forming Factories
Quality Points to Inspect
When you check factory test videos or machine acceptance, focus on these details:
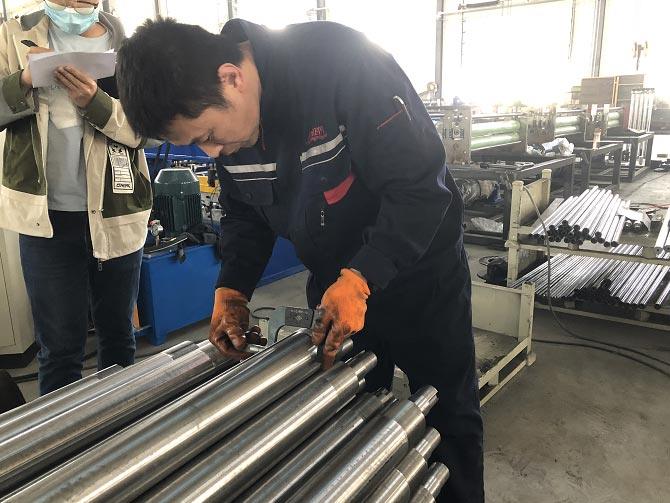
Slit edge condition: Clean, minimal burrs, no paint peeling on PPGI material
Strip straightness: No camber after slitting, otherwise your roll forming machine will track sideways
Recoiling quality: Flat, neat coils without tower shape, loose layers or crushed edges
Knife running stability: No vibration during continuous slitting
Frame rigidity: Heavy welded base frame avoids deflection under full coil load
EPC performance: Automatic edge tracking works reliably for offset coils
Slitting Line Types: Mini / Medium Duty / Heavy Duty
Mini slitting line: Compact, low investment, for small roofing workshops, 0.25–0.8 mm PPGI, 3 ton max coil. Easy to install and occupy small space.
Medium duty slitting line: Most popular for roll forming factories. Handles galvanized, galvalume and prepainted coil, stable for daily continuous production.
Heavy duty slitting line: For thick carbon steel, high tensile steel, large coil weight, steel service center mass processing. Stronger arbor, thicker frame and reinforced tension system.
Advantages of In-house Slitting for Your Roll Forming Business
Flexible width adjustment: You can slit custom narrow strips for special orders anytime, no need to wait for service center schedules
Color & surface consistency: Use the same master coil for all strips of one roof project, no color difference or surface damage from third-party handling
Lower material waste: Optimize nesting layout to minimize edge scrap
Shorter lead time: Raw coil stock arrives, slit on demand and feed directly into your forming machines
Cost control: Cut intermediate service markup, especially for high-volume roofing production
Metal Coil Slitting Line: A Complete Buyer’s Guide for Roll Forming Factories
Frequently Asked Questions
Can one slitting line process both PPGI and carbon steel?
Yes, but you need to inform the supplier. For prepainted coil, the line requires anti-scratch rollers and softer tension settings to protect coating.
How many strips can one line slit at one time?
Depends on minimum slit width and knife layout. Standard roofing lines can make 8–15 strips from a 1250 mm master coil.
What is the difference between slitting line and cut to length line?
Slitting line cuts along the coil length to make narrow strips and rewind coils. Cut to length line cuts crosswise into flat sheets. They serve different downstream processes.
How long is the machine lead time?
Standard medium-duty slitting lines take 25–40 working days. Custom heavy-duty models with special tension or high-precision knife systems take longer. Confirm drawing approval and production schedule in writing.
Does the slitting line need constant operator attendance?
One operator is enough. The operator loads coils, sets parameters, monitors edge quality and changes finished slit coils.
Почему выбирают нас?
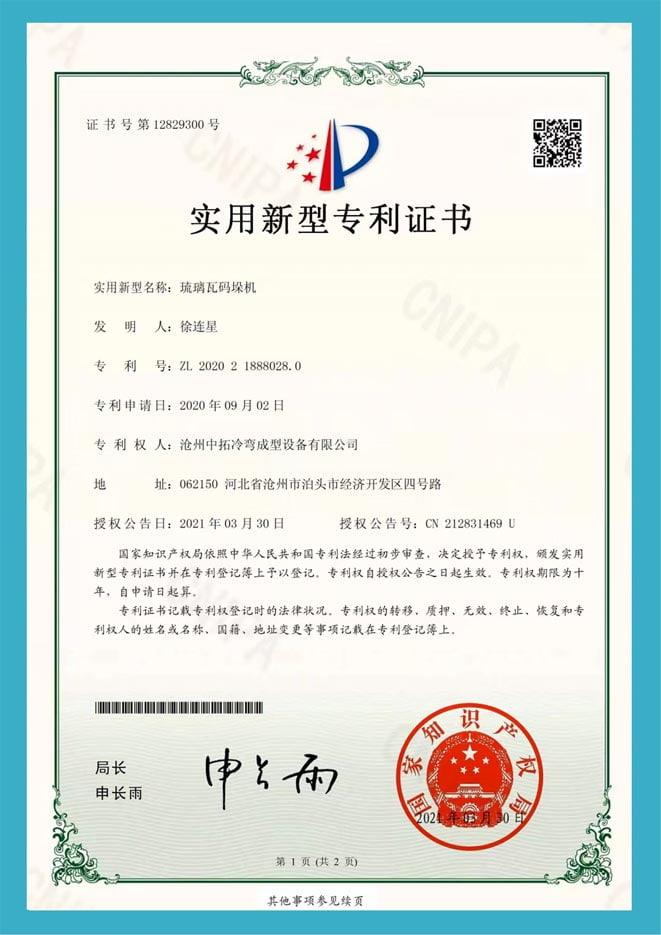
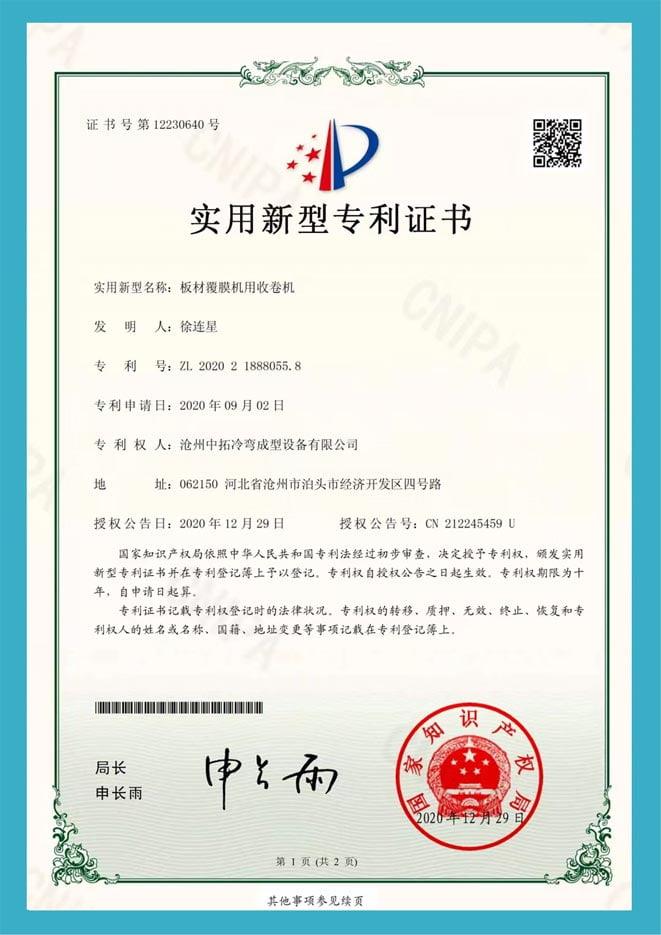
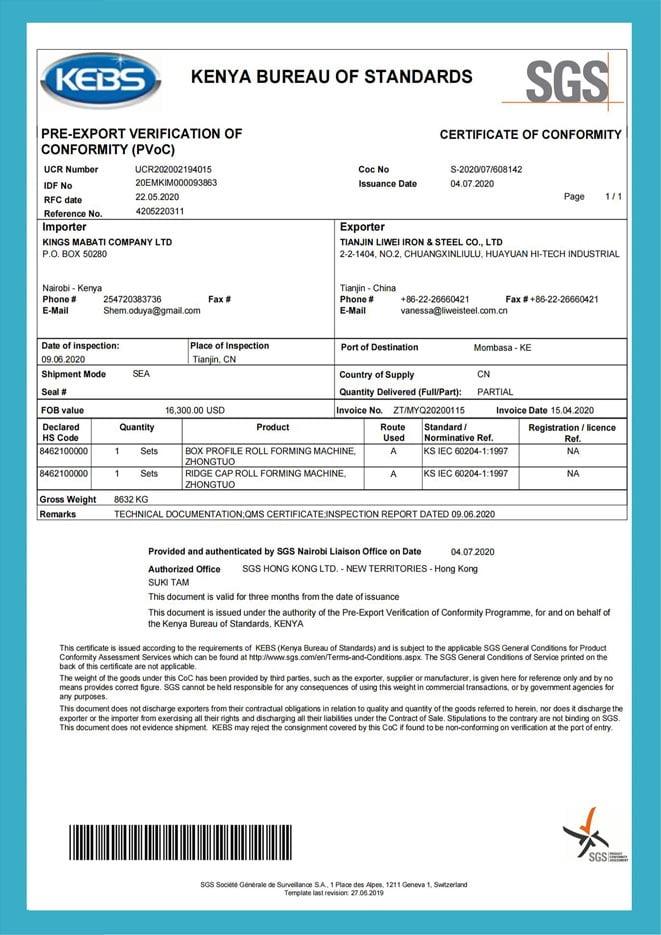
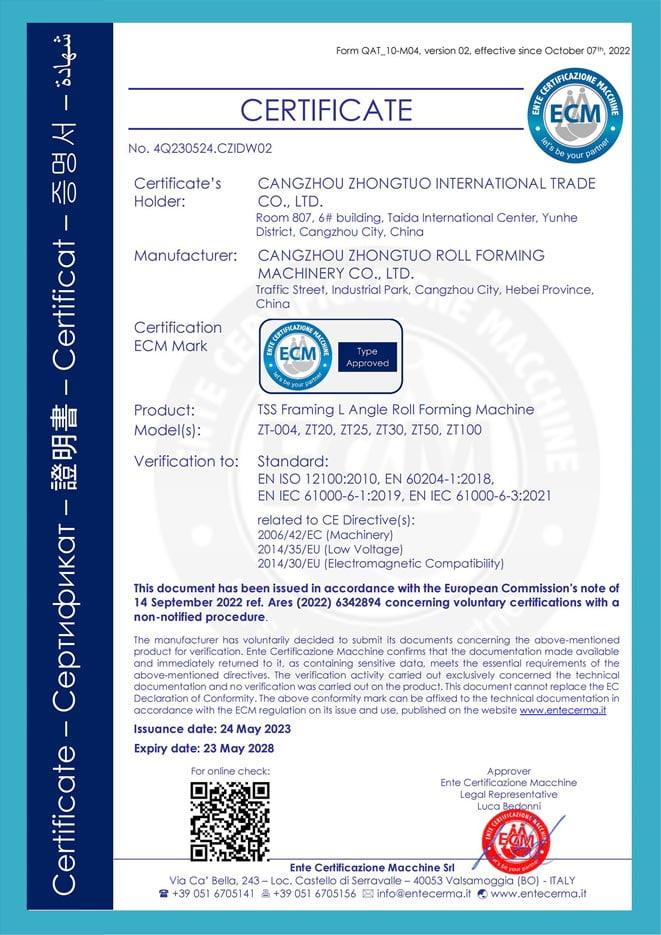
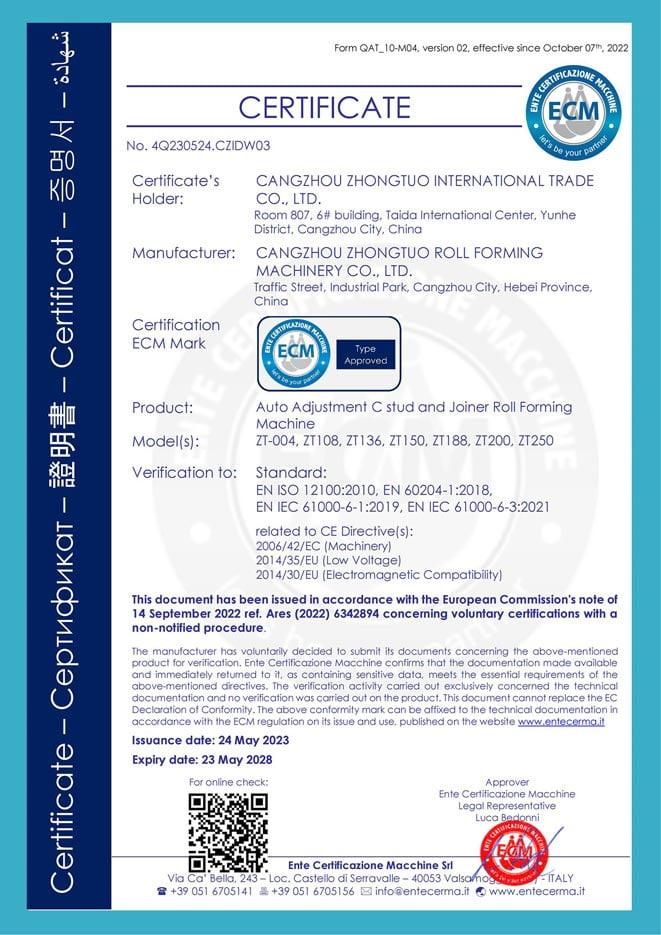
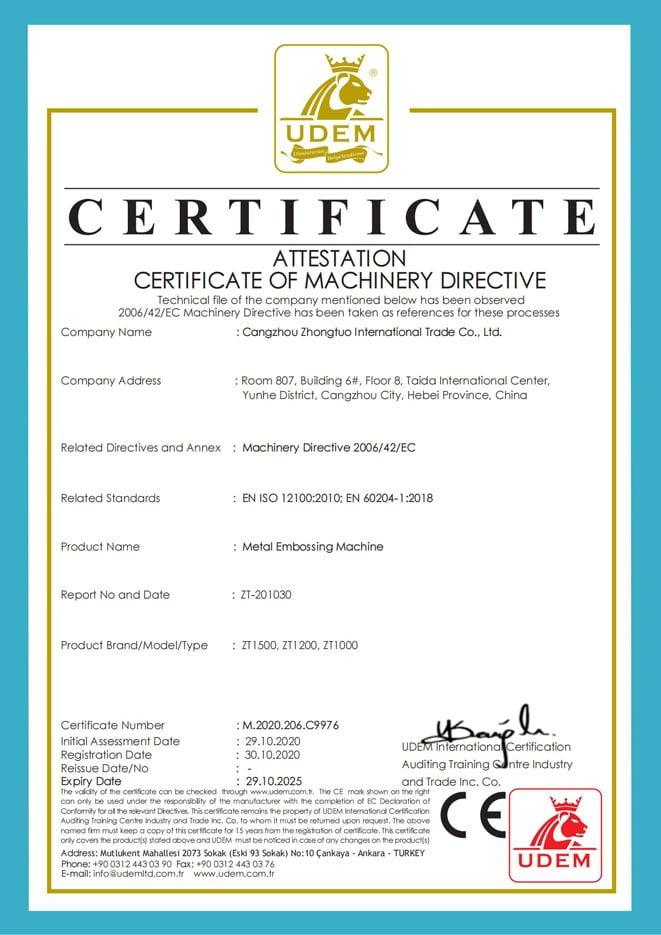
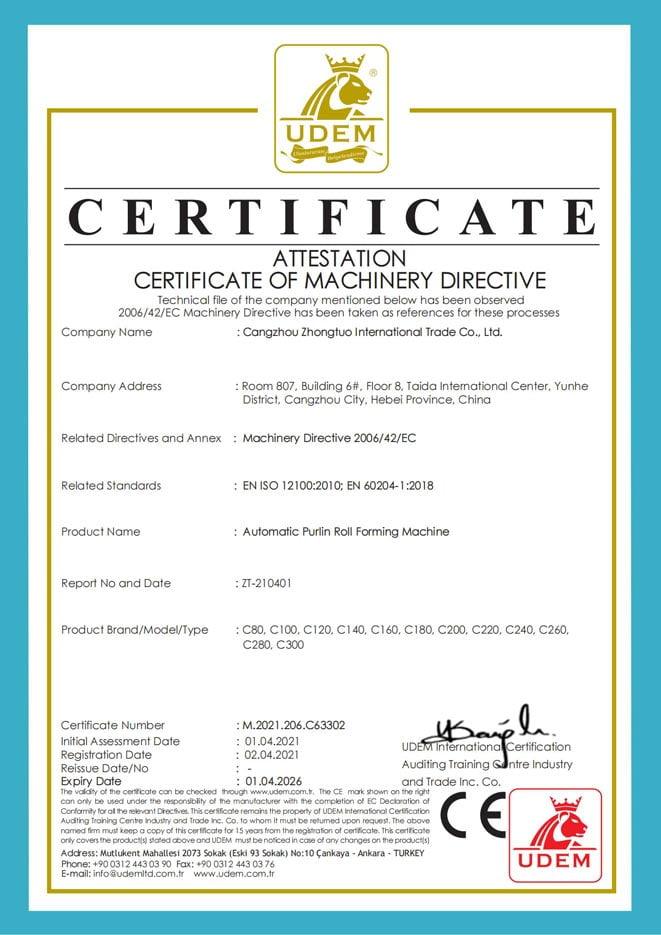
Мы являемся высокотехнологичным предприятием национального уровня. Мы получили сертификацию системы качества ISO9001, европейскую сертификацию безопасности CE, североамериканскую сертификацию CAS и другие. Мы имеем богатый опыт в экспортной торговле, понимая потребности клиентов из разных стран. Между тем, мы можем предоставить клиентам удовлетворительные проектные решения. Наши машины были экспортированы в более чем 150 стран, и мы установили долгосрочные и стабильные отношения сотрудничества с клиентами, и завоевали похвалу клиентов.
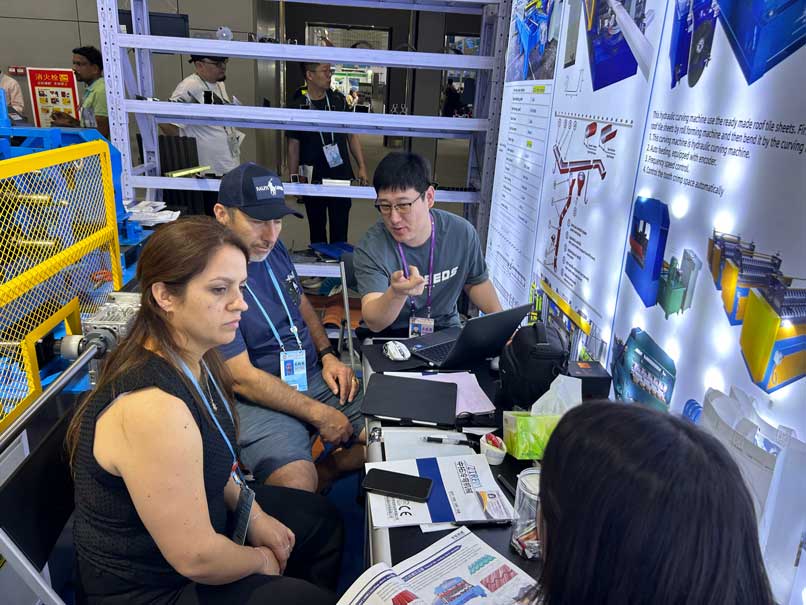
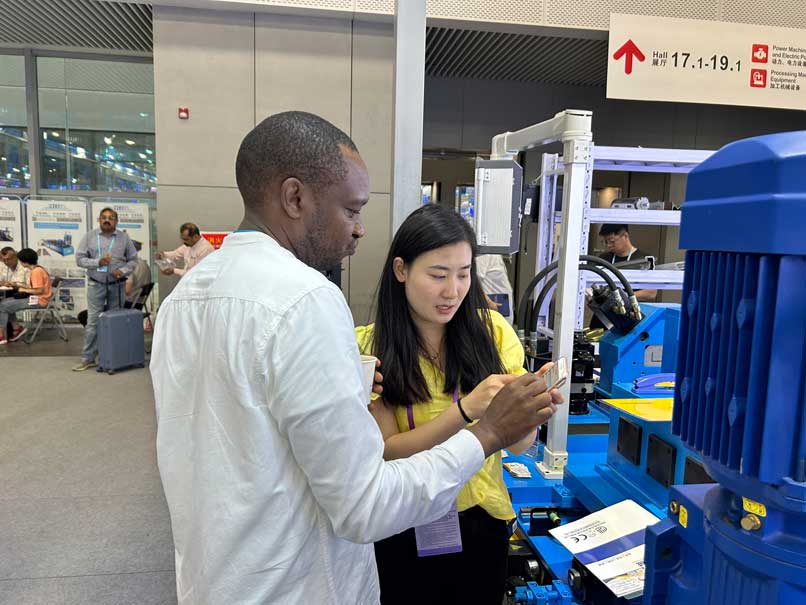
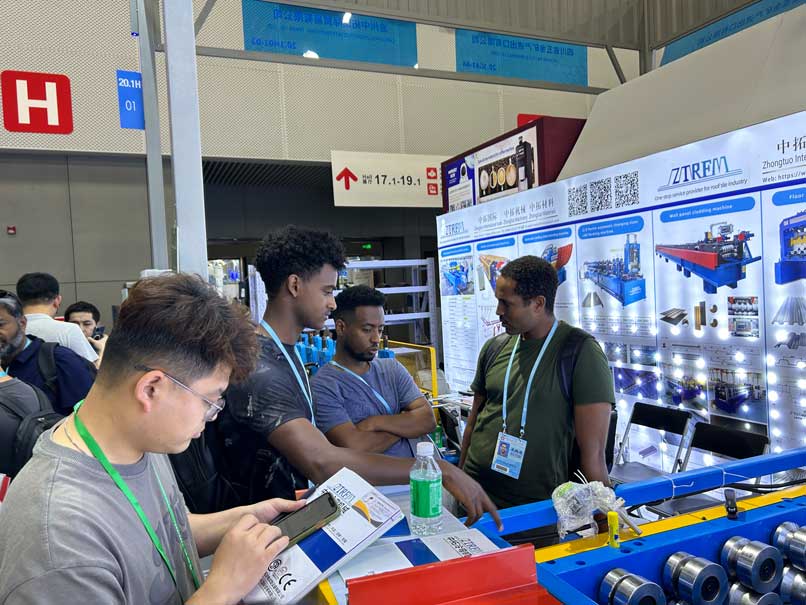
Глобальное доверие: Наши машины для производства кровельных листов, пользующиеся доверием клиентов в более чем 156 странах и регионах, признаны во всем мире за их выдающуюся производительность и надежность.
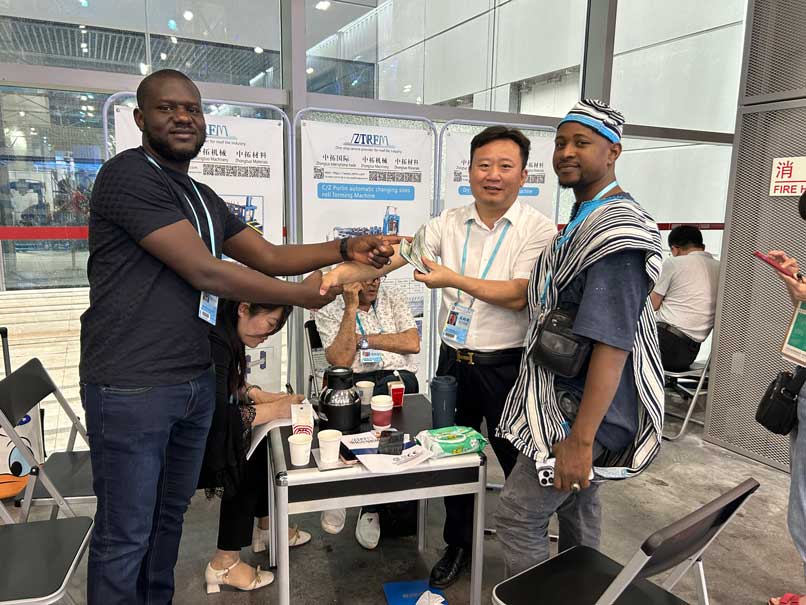
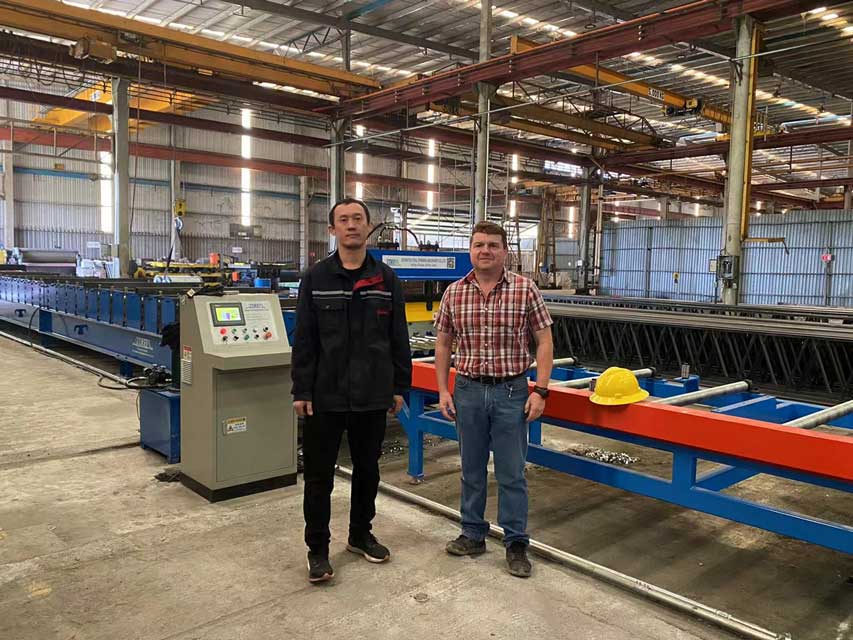
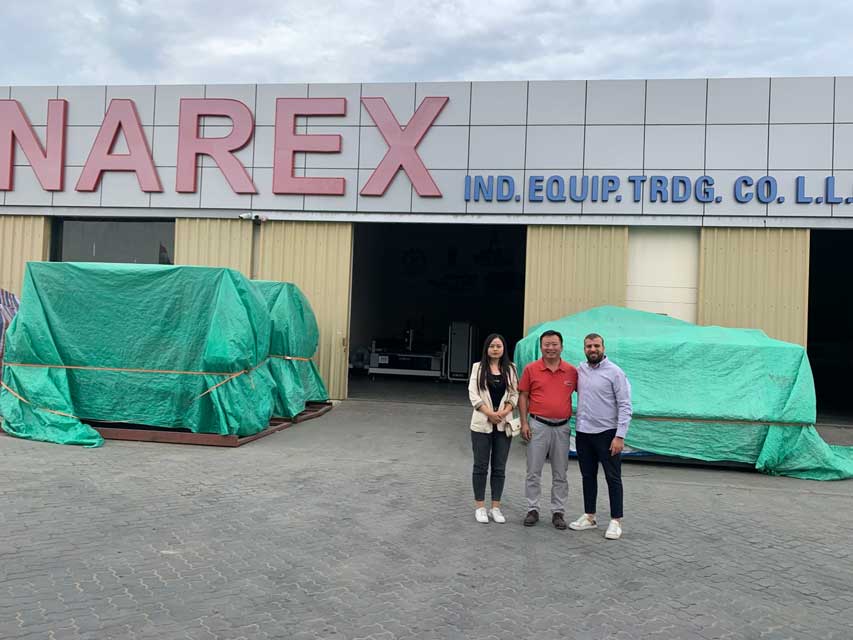
В Замбии, Африке, вальцовочные станки Zhongtuo работают стабильно.
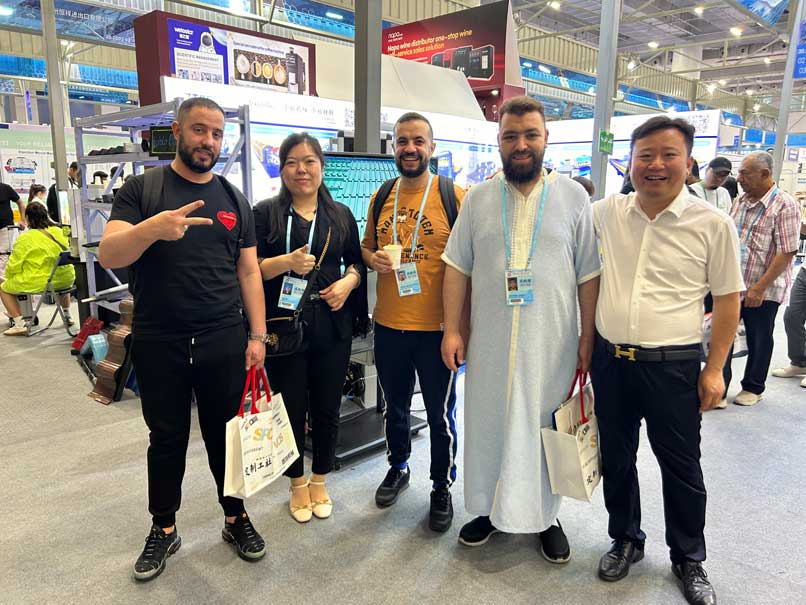
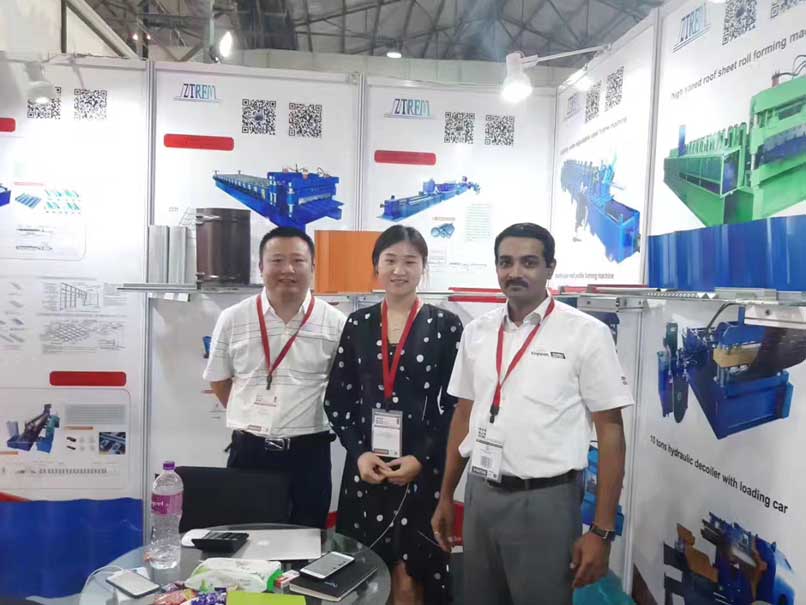
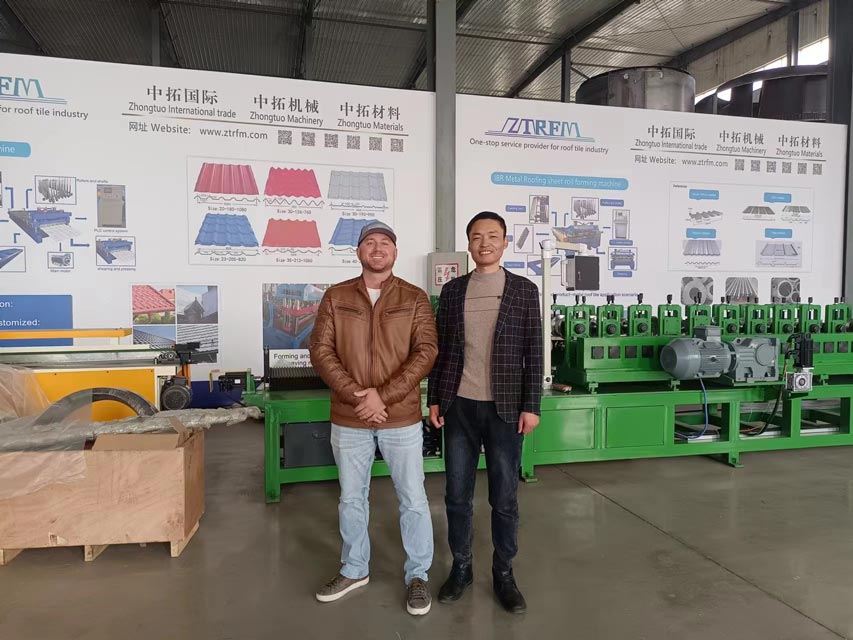
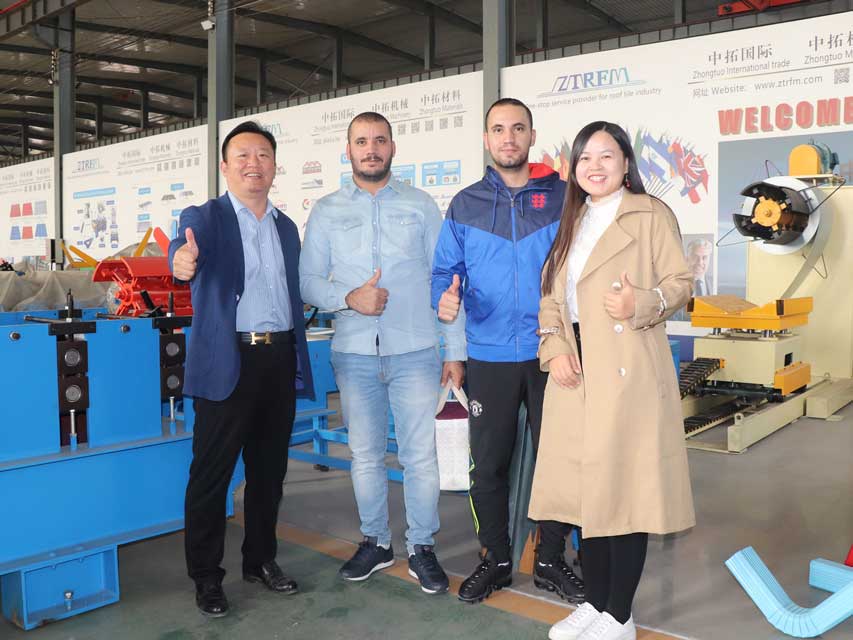
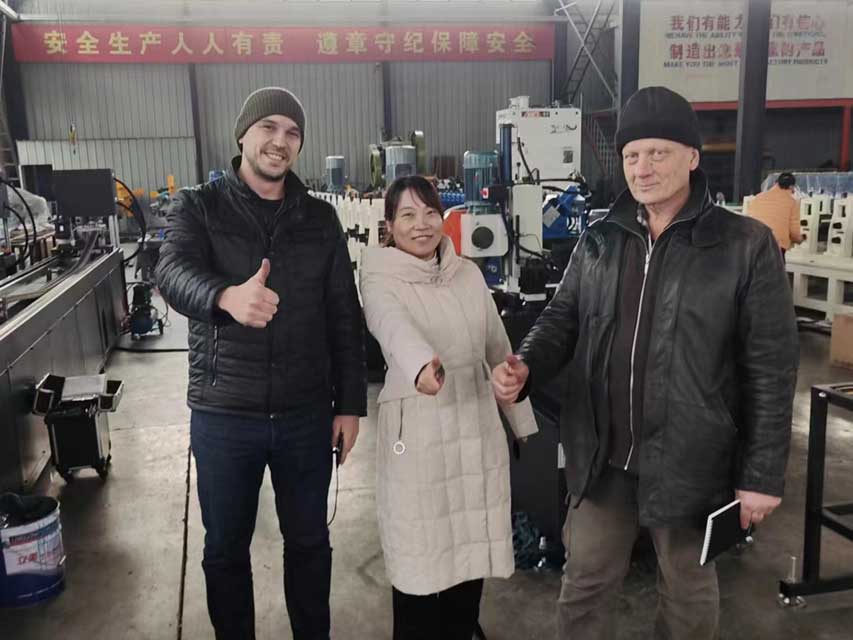
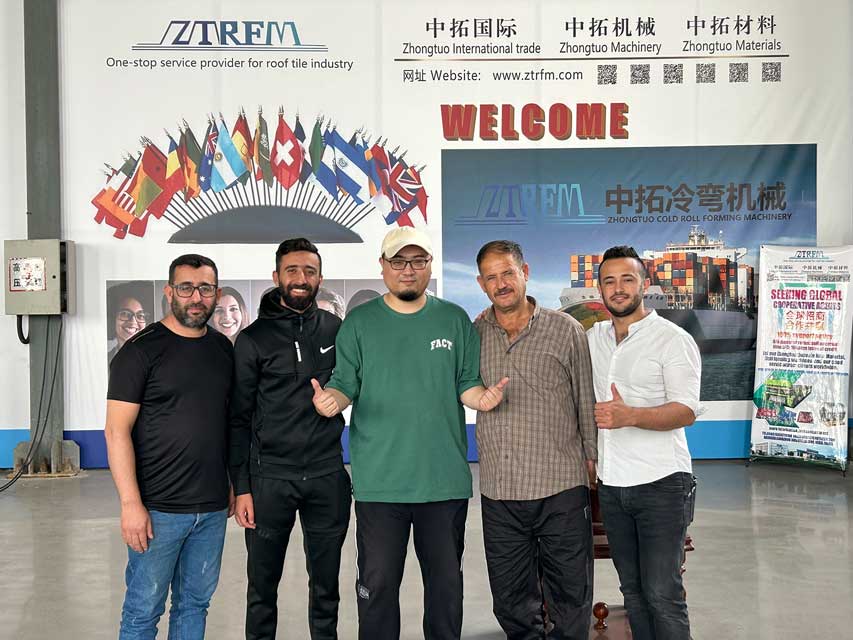
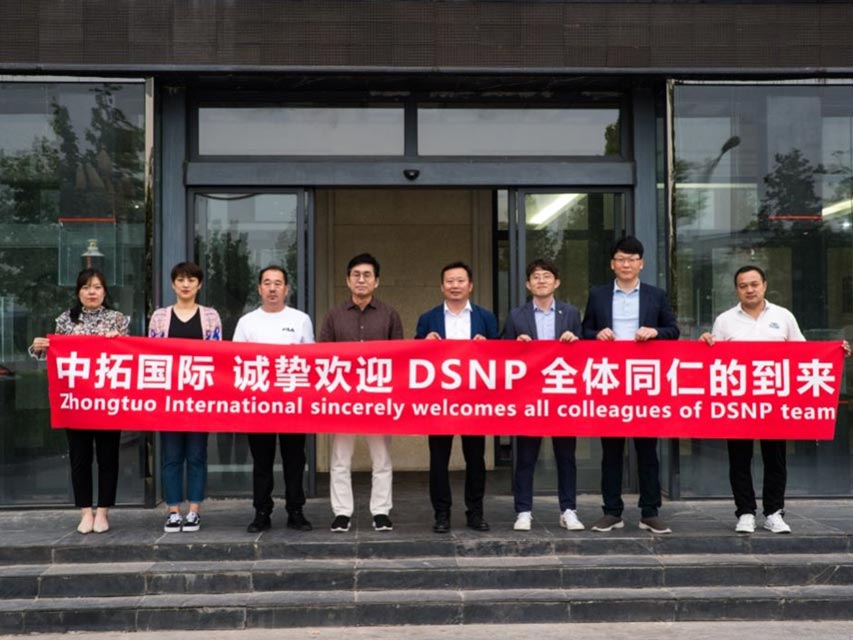
Автоматическая килевая машина CU - монгольские клиенты проверяют заводы и сотрудничают с нами
Линия продольной резки металла Zhongtuo, изготовленная на заказ для клиентов из Бразилии
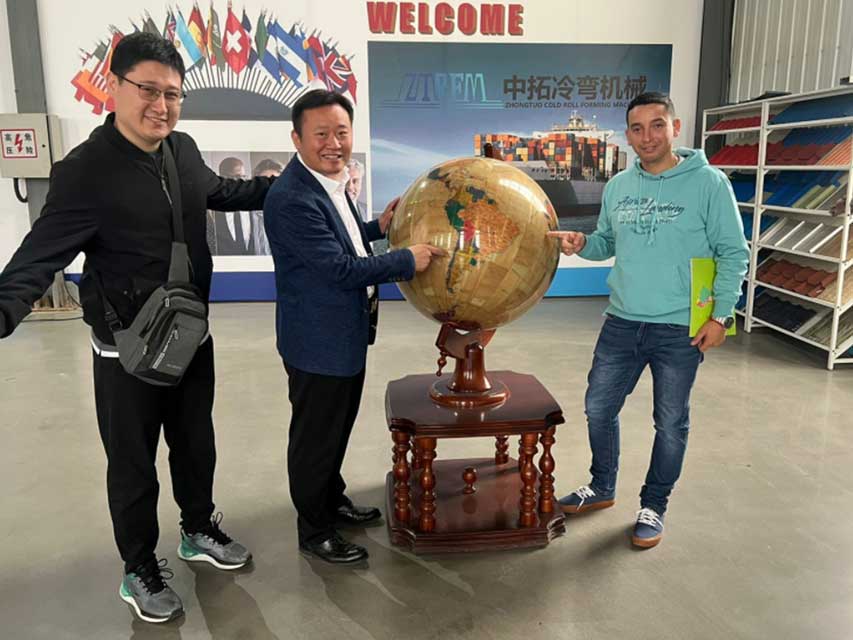
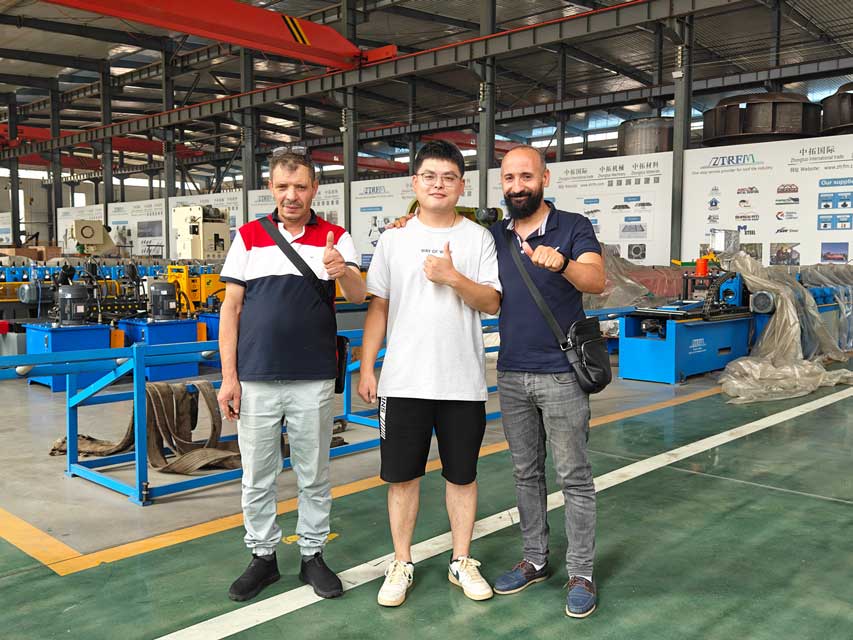
Добро пожаловать в Wedo LLC, чтобы посетить наш завод по производству валковых формовочных машин
Американские друзья вернулись в Cangzhou Zhongtuo Roll Forming Machinery
Металлическая крыша рулонная формовочная машина производить R панели и низкий профиль с автоматической системой укладки
Отзыв клиента о послепродажном обслуживании нашей листогибочной машины
Успешный визит азербайджанских клиентов на наш завод по производству валков!
Zhongtuo Roll Forming Solutions | Индивидуальное оборудование для глобальных отраслей промышленности
Посетите Zhongtuo через систему 360° VR, Цанчжоу Zhongtuo была основана в 2014 году, которая посвящена разработке и производству различных типов машин холодной прокатки. Мы предоставляем услуги ODM, OEM и One-Stop Service. Сырье, оборудование и аксессуары можно приобрести у нас.
Посетите Zhongtuo через систему 360° VR, Цанчжоу Zhongtuo была основана в 2004 году, которая посвящена разработке и производству различных типов машин холодной прокатки. Мы предоставляем услуги ODM, OEM и One-Stop Service. Сырье, оборудование и аксессуары можно приобрести у нас.
OEM/ODM и подгонка по индивидуальному заказу универсальное обслуживание
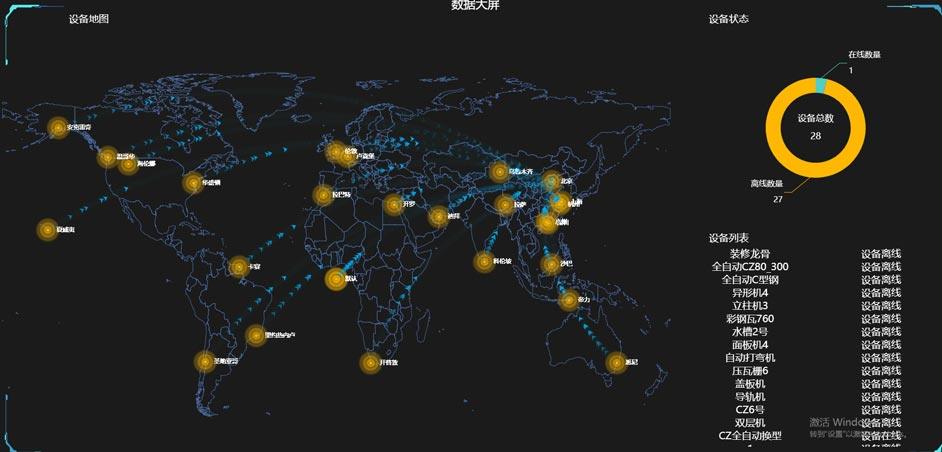
Интеллект в производственном мониторинге: Мониторинг в режиме реального времени для предотвращения производственных аномалий.
Интеллектуальное напоминание: напоминание о неисправностях, напоминание об обслуживании машины и т.д. - эффективно продлевают срок службы машины.
Интеллектуальное послепродажное обслуживание: действительно реализует дистанционное управление послепродажным обслуживанием, нет необходимости отправлять инженеров к клиенту, достигнута экономия времени послепродажного обслуживания и экономия затрат на техническое обслуживание.
Сотрудничество с Siemens-ПЛК управления с глобальной гарантией Siemens.
Купите две машины и получите этот интеллектуальный компьютер в подарок!
Обеспечьте OEM,ODM
1.связь: подтвердите требование покупателя. 2.Техник дизайн: сделать чертеж профилей и 3D машины чертеж 3.определить конфигурацию и производство 4.тестирование перед поставкой
5.упаковка и доставка 6.Техническое руководство 7.Послепродажное обслуживание: услуги по установке сложных машин и регулярное посещение клиентов
Доверяют 95800+ компаний
Для нас большая честь сотрудничать со многими высококачественные предприятия. Благодаря сотрудничеству с нами, они получили сильную поддержку и добились прорыва и развития бизнеса.
0
ISO9001 и CE утверждены
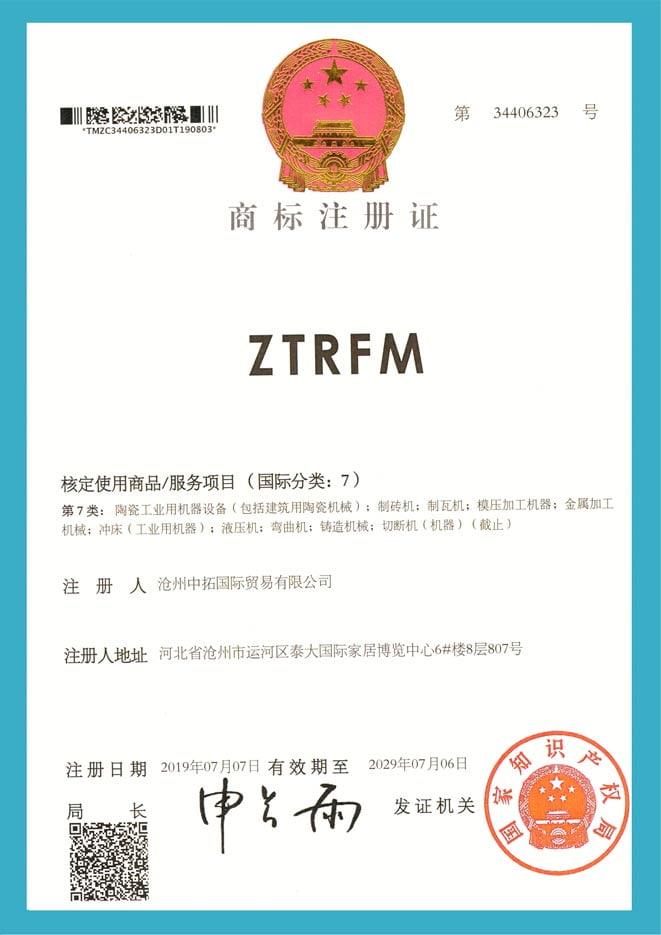
Мы владеем собственной торговой маркой ztrfm, профессиональной командой дизайнеров и техников.
0
Страны-клиенты
Популярные продукты среди пользователей и высоко оцененные.
0
Универсальные решения
от аксессуаров до термопластавтоматов, решая сложные задачи по закупкам.
0
Команда инженеров
У нас есть сильная команда инженеров из более чем 20 человек, мы дадим более точное и быстрое решение.