




Description:Learn how a fence roll forming machine works, key specs (15–30 m/min, 0.5–3 mm), ROI for fence makers, and how to choose the right line for export markets.
A fence roll forming machine is a continuous cold-forming production line that turns steel coils into finished fence components—posts, rails, pickets, mesh frames, guardrail beams, and decorative panels—without manual bending or welding. For overseas buyers, the real question is not “what is it,” but “how much labor, scrap, and lead time does it remove from my fence business.” Based on running roll forming lines for galvanized and PPGI steel in the 0.5–3 mm range, this guide breaks down the process, specs, application fit, and procurement checklist you actually need before paying a deposit.
Traditional fence shops cut flat bar, bend it on a press brake, drill holes on a punch press, then weld or bolt parts together. That model has three hidden taxes:
Positioning error accumulates—every transfer between machines shifts the hole pattern by 0.5–1 mm.
Labor stacks up—a manual line for picket fences often needs 5–6 workers; a roll former needs 1–2.
Scrap grows—press brakes leave dead zones for clamping, wasting 3–6% of coil.
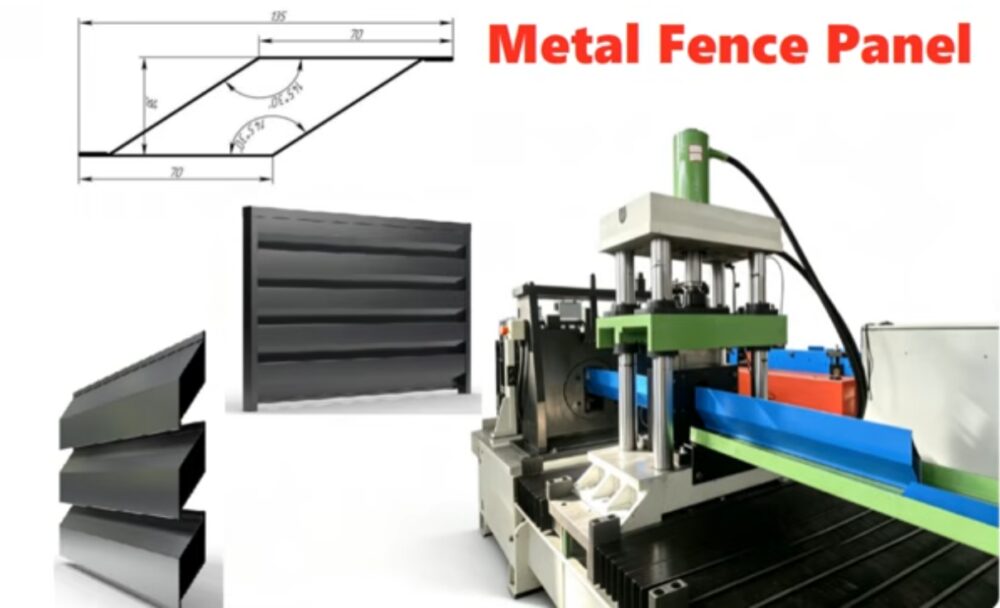
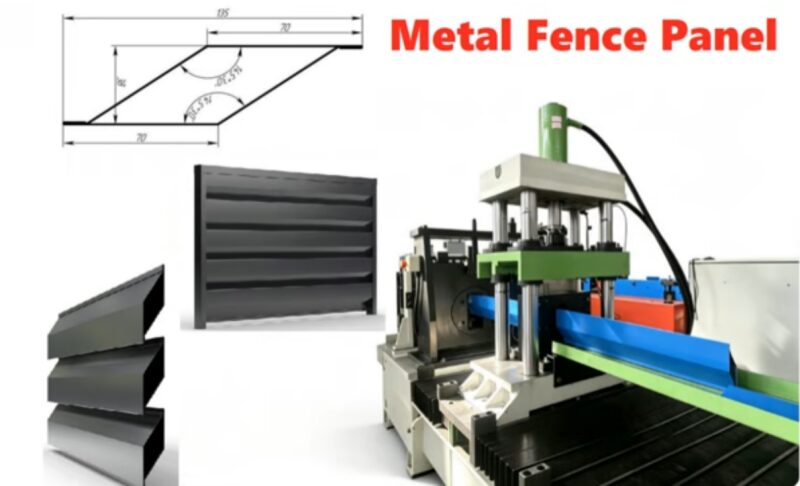
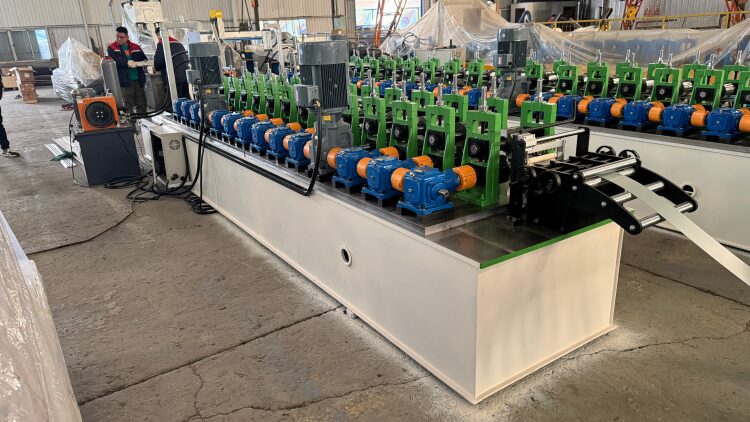
A fence panel roll forming machine merges decoiling, leveling, servo feeding, multi-station rolling, inline hydraulic punching, and flying cutting into one flow. The first panel and the 10,000th panel share the same cross-section tolerance (typically ±2 mm length, profile repeatability within 0.3 mm). That consistency is why highway guardrail suppliers and zinc-steel fence exporters standardize on roll forming instead of job-shop bending.
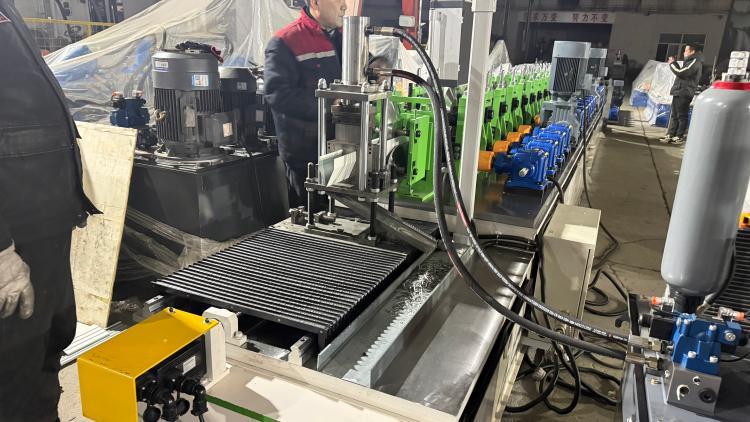
A standard line for metal fence panels follows this sequence:
Hydraulic or manual decoiler holds a 1.5–5 ton coil of GI/PPGI/aluminum/stainless strip.
Feed guide + leveling unit removes coil camber so the strip enters rollers straight.
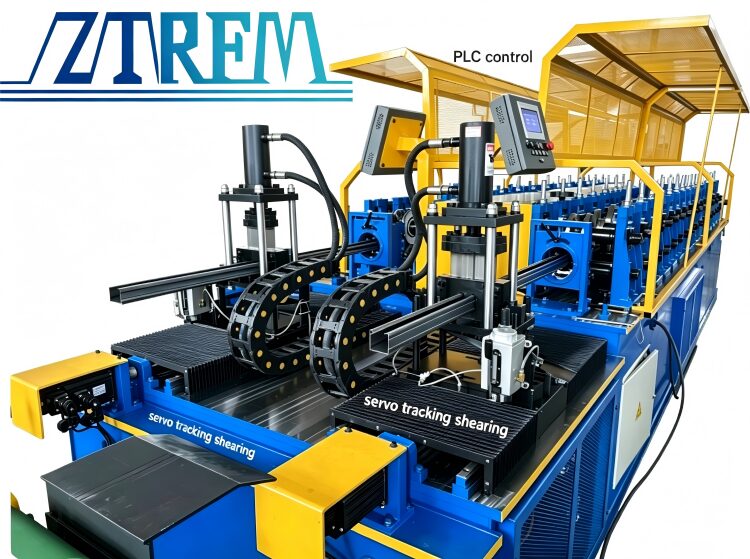
Servo feeder controls pitch when intermittent punching is required.
Roll forming stands (10–20 stations) gradually bend the strip—each stand adds a few degrees until the final profile (C-post, peach post, spear-top picket, double-rail panel) is reached.
Inline hydraulic punch cuts holes, slots, or decorative cutouts while the strip moves.
Flying shear or hydraulic post-cut slices panels to length without stopping the line.
Run-out table + auto stacker collects finished pieces.
Because force is applied gradually over many stands instead of one press stroke, the steel does not crack, and internal stress is released—so panels stay flat after galvanizing or powder coating.
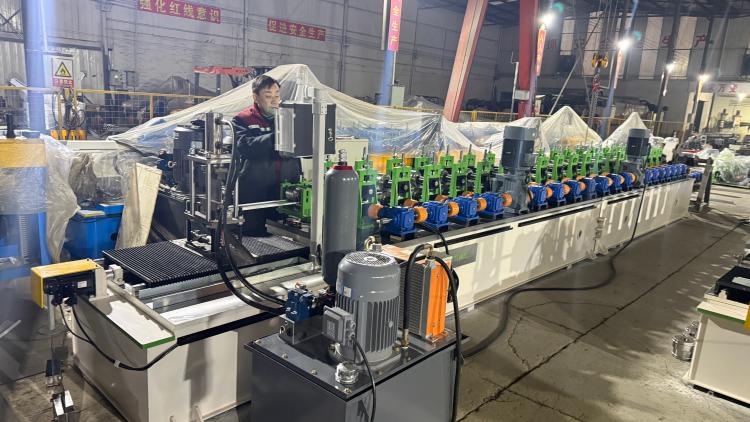
When a supplier sends a quote, do not read the price first. Read these numbers:
| Parameter | Typical range | Why it matters |
| 재료 두께 | 0.5–3 mm (light fence); 0.3–0.8 mm (picket) | Determines shaft diameter and motor power |
| 성형 속도 | 15–30 m/min | 20 m/min ≈ 1200 m shift output for simple profiles |
| 롤러 재질 | 45# forged steel, chrome-plated; or Cr12MoV | Chrome extends life to 3–5 years in GI dust |
| 축 직경 | Φ60–Φ80 mm | Bigger shaft = less deflection on 3 mm steel |
| Main motor | 7.5–15 kW | 7.5 kW fits 0.5–1.2 mm; 11–15 kW for 2–3 mm |
| Cutting | Hydraulic post-cut or servo flying shear | Flying shear keeps line running at full speed |
| PLC | Siemens / Delta / Schneider | Recipe storage saves setup time on repeat orders |
| Tolerance | Length ±2 mm, hole pitch ±0.5 mm | Affects on-site installation speed |
A line rated at 20 m/min with 16 stations and chrome rollers is the workhorse for export-oriented fence makers serving the US, Australia, and GCC markets. Lines below 15 m/min usually mean lighter frame steel and faster roller wear.
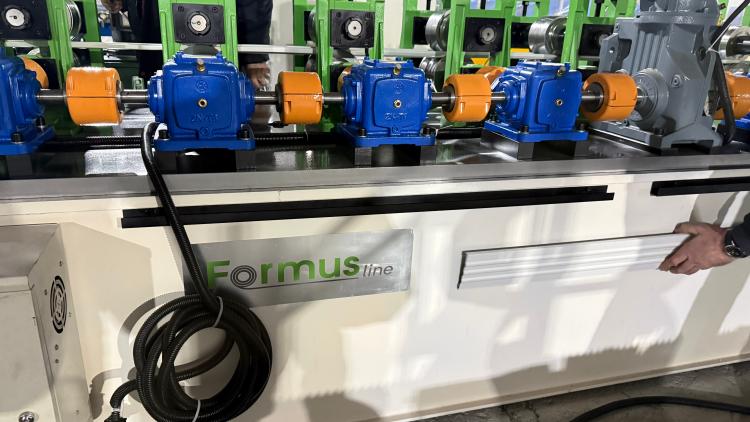
One machine body can serve multiple product lines if you design the roller cassettes correctly:
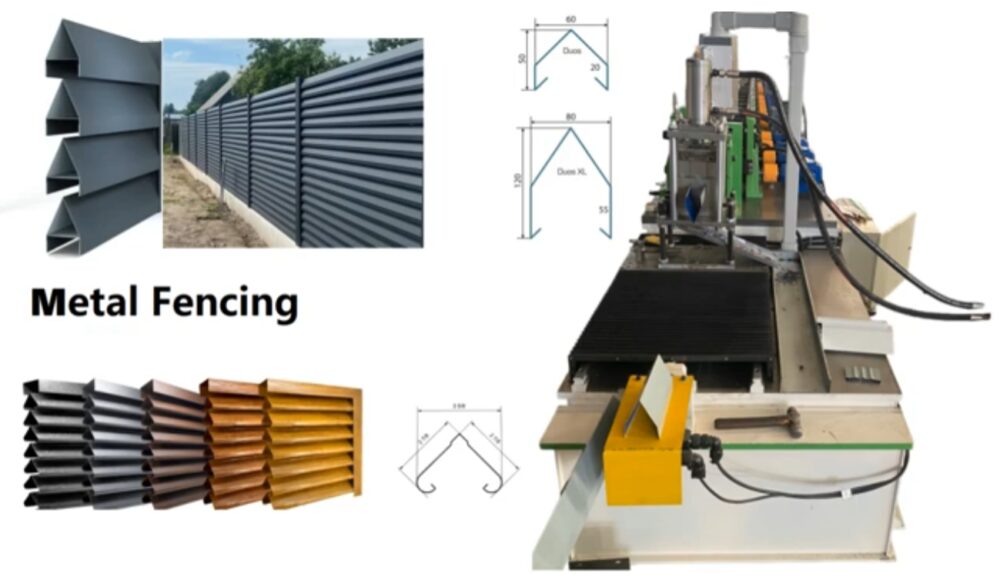
Residential picket fences – spear-top or flat-top vertical bars, 0.6–1.2 mm PPGI.
Zinc-steel assembly fences – rectangular rails + press-fit pickets, no welding.
Peach-shaped (3D) posts – used in EU and Middle East site fencing.
Highway guardrail beams – W-beam or thrie-beam, 2.5–3 mm galvanized.
Agricultural livestock panels – heavier 1.5–2 mm rails with larger mesh frames.
Decorative municipal fences – curved top rail, ornamental rings, park borders.
Changing from a picket profile to a guardrail profile normally takes 4–8 hours of roller exchange, not a new machine. That is the economic argument most importers miss: tooling flexibility turns one CAPEX into three SKUs.
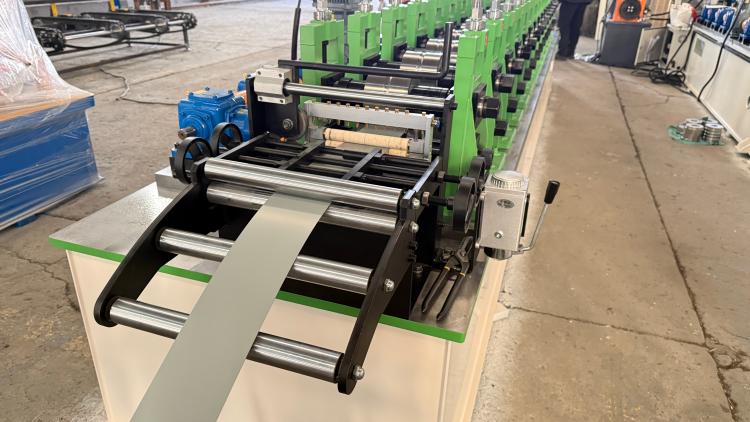
Many overseas inquiries mix up “fence machine” categories. Quick map:
Fence roll forming machine → makes rigid panel/posts from steel coil (flat-to-profile).
Chain link fence machine → weaves wire (1.5–4.5 mm) into diamond mesh, 25–100 mm openings, 60–180 m²/h.
Wire mesh welding machine → spot-welds longitudinal/cross wires into 3D panels.
If your target market buys rigid boundary fences, guardrails, or zinc-steel assemblies, you need roll forming. If you supply sports fields, farms, temporary site fence, chain link is the better sister machine. Serious fence exporters often run both on separate floors.
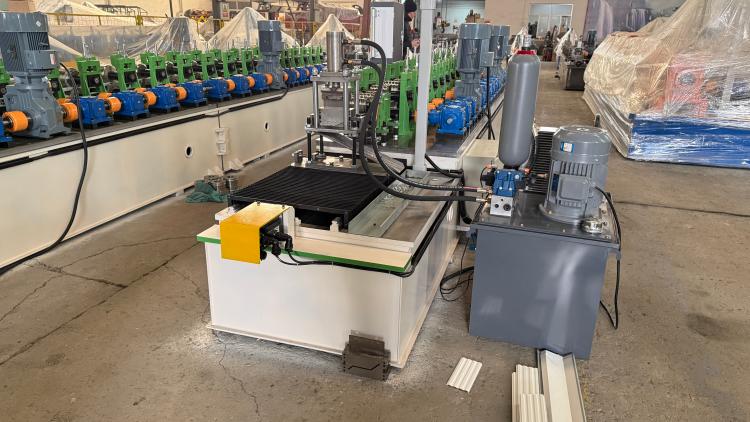
United States: 0.5–1.2 mm PPGI picket fences dominate suburbs; guardrail buyers demand AASHTO-style W-beam and 3 mm min thickness. Voltage 480V/60Hz 3P common.
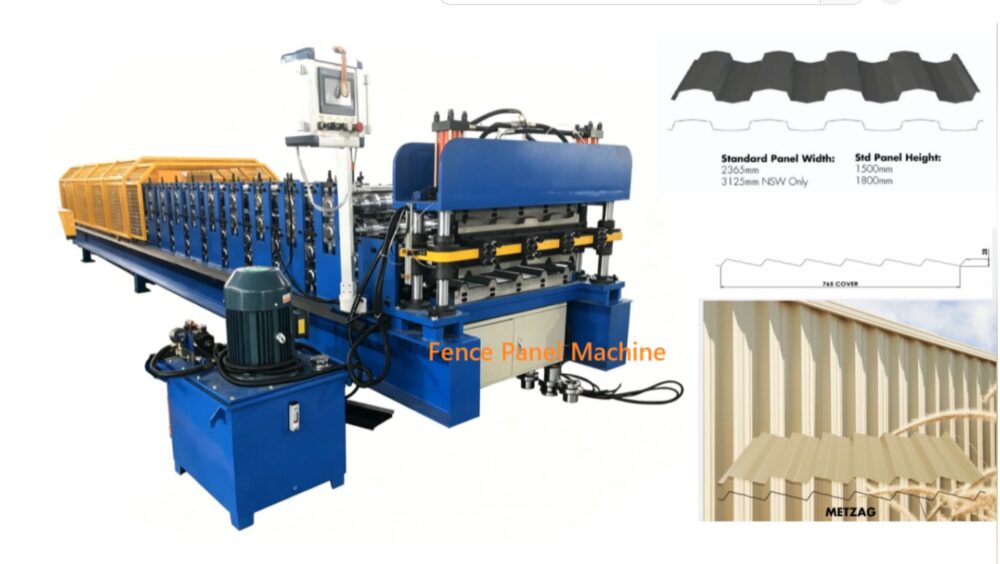
Australia: Colorbond-compatible profiles, 0.55–0.8 mm, 8–10 m panel lengths, AS/NZS coating specs.
GCC: Peach posts + 3D mesh frames, hot-dip galvanized after forming, 50°C storage resilience on PLC cabinet cooling.
EU: CE marking, emergency stop per EN ISO 13850, noise <75 dB, chrome plating waste compliance.
Specify target country in your inquiry—good suppliers pre-wire the PLC, change gearbox ratio, and adjust decoiler width before shipping.
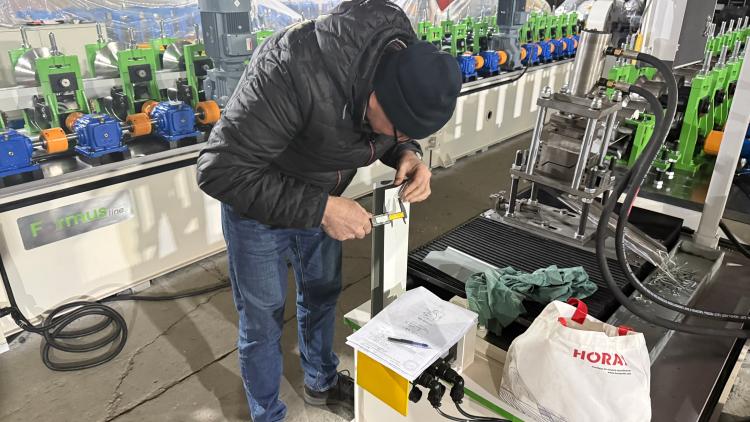
Roll forming machines fail quietly—rollers wear, chains stretch, encoder drifts. Keep these intervals:
Daily: check oil level in hydraulic unit, blow dust off rollers, confirm emergency stop.
Every 500 h: lubricate chain, inspect blade clearance, tighten servo couplings.
Every 1000 h: measure profile pitch with caliper, re-zero encoder if drift >1 mm.
Every 6 months: check chrome layer on rollers; regrind if scoring appears.
Annual: replace hydraulic filter, backup PLC recipes to USB.
Plants that follow this schedule see 10+ year service life on the frame and 3–5 years on roller sets before re-chroming.
A: Same base frame, different roller cassettes and punch molds. Guardrail needs heavier shaft (Φ70+ mm) and 11 kW+ motor, so buy the stronger base if you plan to expand later.
A: For <12 m/min or short panels, hydraulic post-cut is fine. Above 15 m/min, flying shear protects throughput and avoids micro-bends at the cut point.
A: 2–3 days on the PLC touchscreen for a repeat-profile shop. New profile setup still needs a technician for roller gap tuning.
A: Yes, but dirty or unevenly coated coil scratches rollers faster. Keep coil straps off the strip path and level the feed.
A: Standard non-custom line: 25–35 days FOB; customized 45–60 days. 20GP per line is typical for mid-size models.