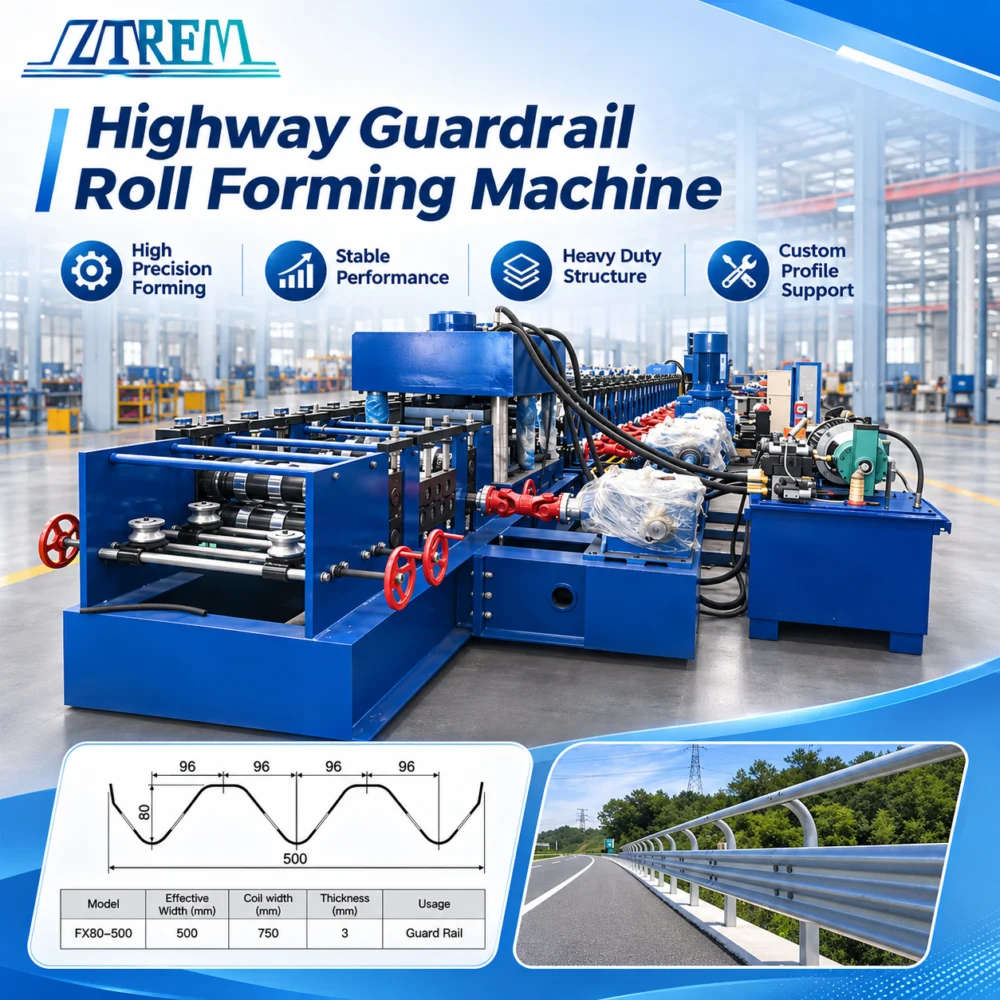
Fully Automatic Highway Guardrail Rolling Forming Machine
Two Wave and Three Wave Guardrail By One Machine Rolling Forming Machine
High-Speed Guardrail Roll Forming Machine
When buyers compare a high-speed guardrail roll forming machine, the first number they look at is the forming speed. That is understandable — but the number on the quotation sheet and the number your forklift actually moves every shift are rarely the same. A line rated at 25 m/min can deliver 800 metres an hour on one factory floor and 1,300 on another, with the same motor, the same stations and the same PLC.
This article explains what high speed means for a W-beam or thrie-beam production line, where the speed physically comes from, what it costs you when the line runs fast, and how to test a supplier's claim before you sign. It is written for road-safety product manufacturers, steel fabricators and procurement engineers who need a line that runs at its rated speed for eight hours, not for five minutes during a demonstration.
High-Speed Guardrail Roll Forming Machine
What makes a guardrail line "high speed"
The market splits guardrail roll forming lines into three broad bands. Conventional lines form and cut at roughly 8–15 m/min and are usually built around a stop-start cutting cycle. High-speed lines run continuously at about 20–30 m/min, with a flying shear or servo flying cut that follows the beam instead of stopping it. The fastest configurations, built for large export contracts, reach 30–55 m/min — but only when the punching, cutting, stacking and coil-handling side of the line is engineered to keep up.
That third band is where most misunderstandings begin. A machine does not become "high speed" because a larger motor is fitted. Speed is a system property: if the punch press needs two seconds per hole pattern and the beam arrives every 1.4 seconds, the line slows to the punch, and the extra motor capacity is wasted.
From coil to stacked beam: what is actually inside the line
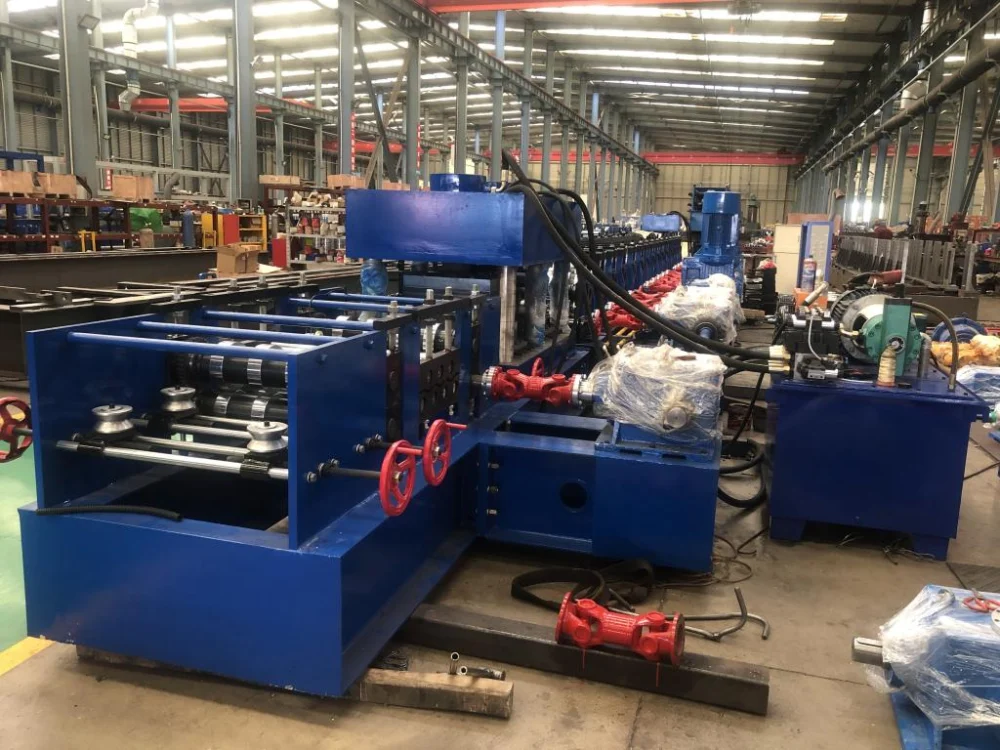
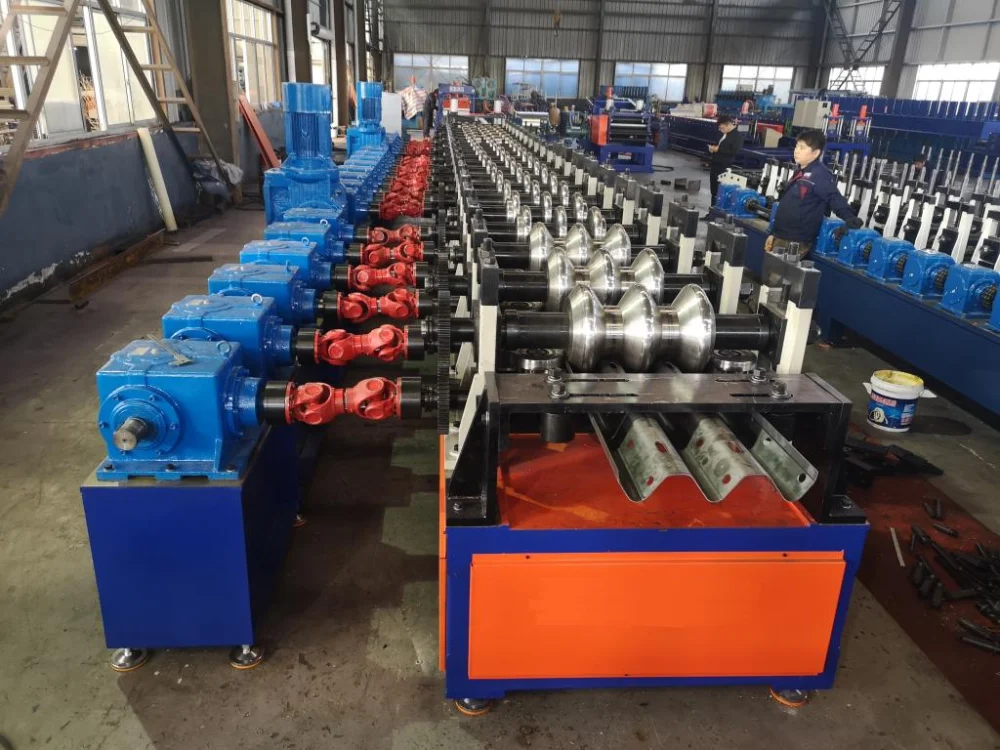
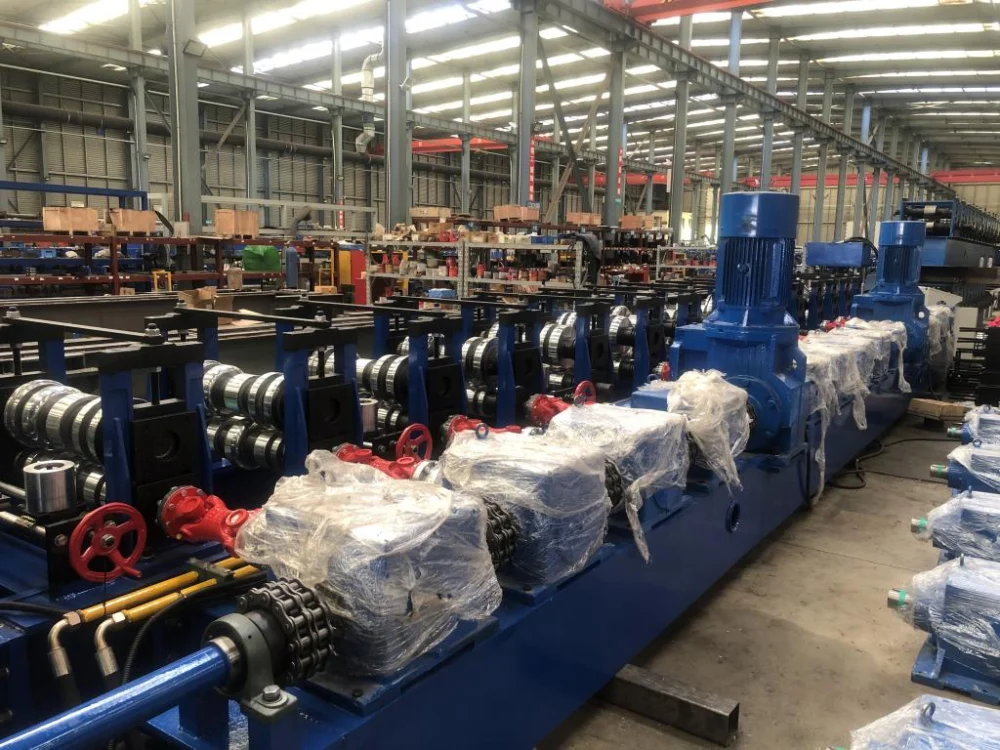
A complete high-speed guardrail production line normally contains the following units, and each of them has a role in whether the rated speed is reachable in production:
Decoiler and coil car — handles coils of roughly 8–10 tonnes, with a hydraulic expansion mandrel and a coil car that loads without a crane.
Entry leveler — a seven-roller leveler removes coil curvature and cross-bow before forming; skip it and every profile defect downstream traces back to the coil.
Servo feed and loop control — matches coil pay-off to line demand so the strip never drags or surges into the first station.
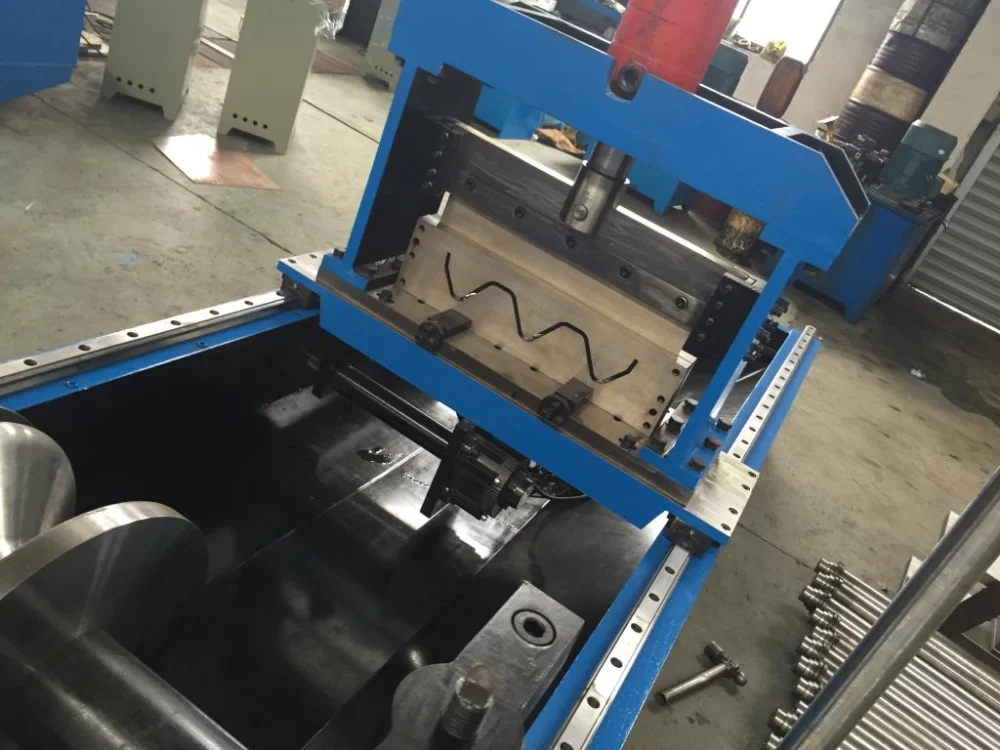
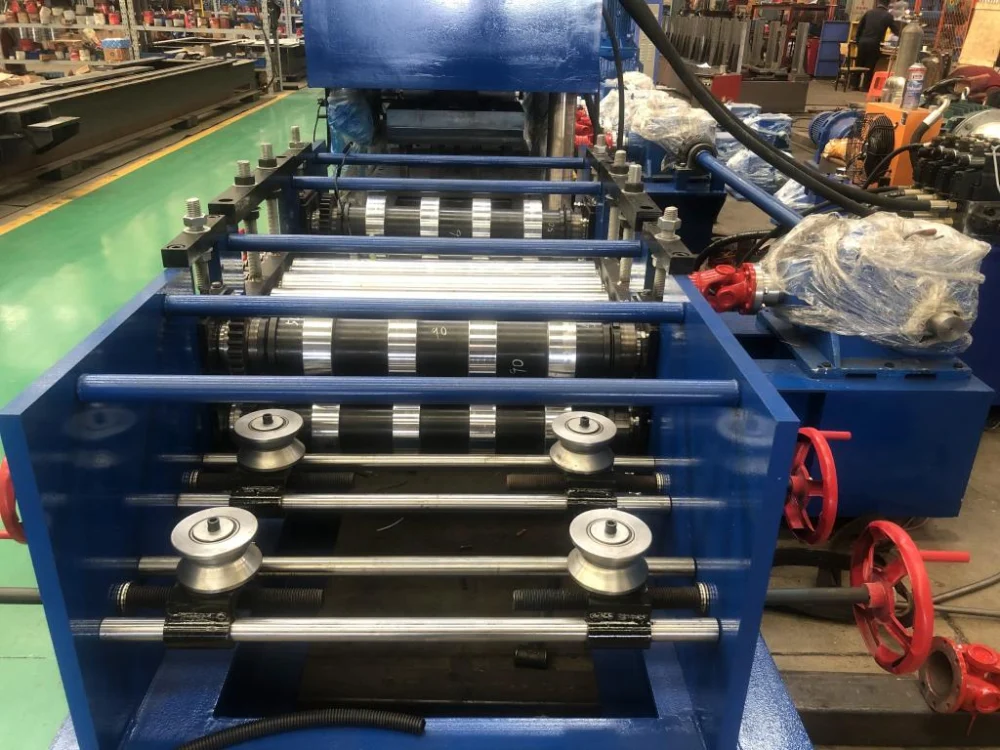
Roll forming stations — typically 16–22 stands for a W-beam, more for a thrie-beam or a combination line. Stations do the shaping; the count decides whether the profile is formed gently or forced.
Inline hydraulic punching — punches post holes, splice holes and, on some profiles, slot patterns while the strip moves or during a controlled dwell.
Flying shear or servo flying cut
Run-out table and stacker — receives 3.2 m or 4.3 m beams at speed without scratching the galvanized surface.
Hydraulic power unit, PLC and HMI — one recipe per profile, with length, hole pattern and speed stored as parameters rather than set by hand.
Guardrail is a safety product, so the line also needs full guarding, emergency stops and interlocked access doors. Those are not optional extras; in most export markets they are part of the acceptance inspection.
The only speed figure that matters: finished metres per hour
Convert the rated speed into hourly output and the picture becomes honest. At 25 m/min, the theoretical ceiling is 1,500 metres per hour. No plant reaches the ceiling, because production time is consumed by coil changes, cut-length changes, punching dwell, stacking and the occasional stoppage.
A realistic planning factor for a well-run high-speed line is 75–85% of theoretical output, which puts a 25 m/min machine at roughly 1,100–1,300 finished metres per hour. A 30 m/min line lands near 1,350–1,500. If a supplier quotes output above the theoretical figure, the arithmetic is wrong, not the machine.
Where the hours actually go:
Coil changes — a 10-tonne coil at 3 mm thickness yields a few hundred metres; two operators need several minutes per change unless a double-head decoiler is specified.
Punching — dense hole patterns, or a punch that runs in dwell mode, pull the line below its forming speed.
Cutting and stacking — a shear that cannot cycle at line speed becomes the bottleneck; so does a stacker that needs manual straightening.
Changeover and scrap — profile changes, strip threading and the first few metres of scrap at start-up.
Run the same calculation for a conventional 10 m/min line and the difference is clear: about 600 metres theoretical, perhaps 450–500 in practice. That gap — roughly 600–800 metres per hour — is what the price premium for a high-speed line is actually buying.
High-Speed Guardrail Roll Forming Machine
Engineering that lets the line hold speed without losing the profile
Speed only counts if the beam still passes inspection. Three design decisions separate a line that runs fast from a line that runs fast badly.
Forming stations and drive layout. At 25–30 m/min, strip passes each stand in a fraction of a second, so the deformation has to be gentle. More stations, each taking a smaller bend, reduce edge wave and prevent the wave depth from springing back after the rolls. All rolls should be driven — top and bottom — because a friction-driven upper roll slips at speed and marks galvanized surfaces.
Roll material and rigidity. Rolls are commonly made from GCr15 bearing steel or Cr12 mould steel, quenched to HRC 58–63, with hard chrome plating where surface finish matters. The frame and stands must be stiff enough that the forming load does not deflect the shaft line; deflection shows up as inconsistent beam depth along the length.
Motion synchronisation. The servo feed, the flying shear and the punch must share one motion profile. When they are not synchronised, the cut length drifts, holes land a few millimetres off, and the operator compensates by slowing the line — which is exactly the speed you paid for.
Profiles, materials and standards the line must handle
Most export enquiries cover two profiles. The two-wave W-beam is the global standard, around 310–312 mm wide with an 83 mm wave depth. The three-wave thrie-beam is wider and taller and is used where a higher containment level is required. A combination line with quick-change cassettes can produce both; a dedicated line produces one, faster and cheaper.
Typical working range:
Strip thickness — 2.5–4.0 mm, covering AASHTO Class A (2.67 mm) and Class B (3.43 mm) base metal, plus local variants.
Beam length — 2,320, 3,200 and 4,320 mm are the common lengths, with custom lengths set through the PLC.
Material — Q235B, Q345B, S235JR and S355JR, supplied black or pre-galvanized. Zinc coating in the 275–610 g/m² range is normal for pre-galvanized coil.
Standards — AASHTO M180, EN 1317, AS/NZS 3845 and comparable national specifications, depending on the destination market.
Two practical notes. First, pre-galvanized strip is less forgiving than black strip: roll surfaces, guide entries and the stacker all have to avoid scratching, because a scratch through the zinc layer becomes a corrosion point that no rework can fix. Second, if the same line must run both 2.5 mm and 4.0 mm strip, the roll gap adjustment and the punch tonnage have to be specified for the thickest material from the start; retrofitting a heavier hydraulic unit later costs far more than ordering it correctly.
High-Speed Guardrail Roll Forming Machine
What to check at full speed, not at low speed
Inspection at 5 m/min proves the tooling is correct. Inspection at 25 m/min proves the line is sellable. The checks that matter:
Wave depth and beam width — measured at the start, middle and end of a coil, not on one sample.
Length accuracy — cut-to-length tolerance across a run, especially after a speed change.
Camber and twist — a beam that looks straight on the stacker can twist once it is lifted; check on a flat table after cooling.
Hole position — post holes and splice holes relative to the beam end, and hole-to-hole spacing.
Surface — roll marks, edge burr, and zinc damage on pre-galvanized material.
Consistency over time — sample every 30 minutes through an eight-hour run; drift is a design or thermal problem, not an operator problem.
Changeover: one line, W-beam and thrie-beam
Mixed export orders are common, and a line that needs a full day to change profile quickly becomes a line that runs one product. Quick-change cassette designs address this by making the forming stands a mechanical swap: the W-beam cassette comes out, the thrie-beam cassette goes in, and the punch dies, shear blades and PLC recipe change with it.
What still takes time is the part buyers underestimate — alignment and first-off approval. Budget for a few hours per change, not a few minutes, and ask the supplier to demonstrate a changeover during the acceptance test rather than describing it in the brochure.
Running cost and payback
For a typical high-speed line, the main drive is in the 45–75 kW range and the hydraulic unit another 15–22 kW, so connected load sits near 60–100 kW. Energy per finished tonne is lower on a high-speed line than on a slow one, because idle time and re-heating of the hydraulic oil are reduced, but the connected load is higher and the local supply must be checked before installation.
Labour is the clearer saving. A high-speed line with automatic stacking runs with one operator and one helper; a conventional line often needs two operators plus a third person handling cut beams. On a two-shift operation that difference is a full wage per day, every day, which is usually the fastest part of the payback calculation.
Scrap and tooling life are the variables to watch. A line pushed beyond its stable speed produces more edge wave and more rejects; a line run at 80% of its ceiling usually produces less scrap than one run flat out. The right operating point is a commercial decision, and the PLC recipe should make it easy to hold.
High-Speed Guardrail Roll Forming Machine
How to verify a supplier's claim
Ask for an acceptance test that runs the line the way you will run it, and put the conditions in the contract:
A continuous run of at least four hours, ideally eight, from coil to stacked beam at the declared speed.
Measured output in finished metres, with the coil weight consumed recorded at the same time — this exposes any optimistic conversion.
Dimensions and hole positions sampled through the run, with the report attached to the acceptance document.
Scrap counted, not estimated.
A profile changeover demonstrated, timed, with the first-off beam measured.
An unedited video of the run, plus contact details of two customers running the same model.
If a supplier will only demonstrate at half speed, or will only show a video of a single beam, treat the speed figure as a design target rather than a delivered capability.
Specification checklist before you request a quotation
Send these ten items and the quotation becomes comparable instead of decorative:
Profile drawing with wave geometry and tolerance, for W-beam and thrie-beam if both are required.
Strip thickness range and material grade.
Coil width, coil weight and whether the coil is black or pre-galvanized.
Beam lengths and hole patterns, with a drawing of the end treatment.
Required finished output per shift, and the shifts per day.
Available floor space and the layout direction of the line.
Power supply: voltage, phase, frequency and available capacity.
Destination standard and any third-party inspection requirement.
Preferred PLC and electrical component brands, and the maintenance team's familiarity with them.
Spare parts, training and commissioning scope expected in the offer.
High-Speed Guardrail Roll Forming Machine
Frequently asked questions
What is a realistic speed for a high-speed guardrail roll forming machine?
Forming speeds of 20–30 m/min are the normal high-speed band, with flying-shear configurations reaching 30–55 m/min on large lines. Finished output is typically 75–85% of the theoretical figure once coil changes, punching and stacking are counted.
Can one line make both W-beam and thrie-beam?
Yes, with quick-change cassettes and matching punch and shear tooling. Expect a few hours per change including alignment and first-off approval, not minutes.
What thickness range should I specify?
Cover the thickest material you will realistically sell. A 2.5–4.0 mm range handles AASHTO Class A and Class B beams and most export specifications; specifying 4.0 mm from the start is cheaper than upgrading the rolls, shafts and hydraulics later.
Does the line run pre-galvanized coil?
Yes, and most export production does. The requirements are hardened, chrome-plated roll surfaces, protected guide entries and a stacker that does not drag the beam.
How much floor space does it need?
A complete line from decoiler to stacker usually occupies a strip roughly 35–55 m long and 6–8 m wide, depending on beam length, stacker type and whether a double-head decoiler is included. Confirm the layout drawing against your building before ordering.
What should the acceptance test include?
A continuous run at declared speed, measured output, sampled dimensions and hole positions, counted scrap, a timed changeover demonstration and customer references. Anything less leaves the speed claim unverified.